

Featured OEM Precision Components
High-Precision PM & MIM Product Lineup
Direct from Ningbo manufacturing hub. Sintered steel, stainless alloys, ceramic tubing, and complex metal injection molded components certified to IATF 16949 standards.
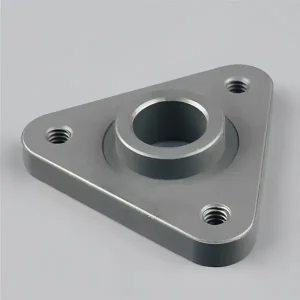
China Sintered Powder Metal Water Pump Flange Supplier Manufacturers, Factories

Wholesale SIM Slot by Metal Injection Molding Manufacturer, Manufacturers

Wholesale PriceList for Custom Sintering Metal Injection Molding MIM Hardware for CNC Machinery Auto Parts Manufacturer, Factories
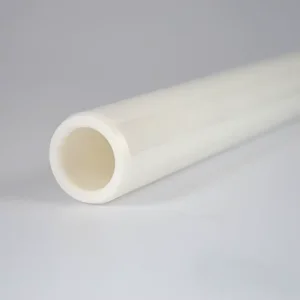
Wholesale Zirconia Ceramic Tube Manufacturer, Factories

Wholesale Top Quality OEM High Precison 304 Stainless Steel Parts China Metal Fabrication Factory Suppliers, Factories

China Europe style for Aluminum Actuator End Cup Die Casting Manufacturers, Factories

Wholesale Wholesale ODM Powder Metallurgy Diesel Engine Oil Pump Rotor Manufacturer, Manufacturers
Global Metallurgy Market Dynamics
State of Global Powder Metallurgy & China's Industrial Role
Analyzing market expansion, structural alloy demands, near-net-shape manufacturing efficiencies, and technological shifts across key OEM sectors worldwide.
Macro Economic Trends & Demand Drivers
The global powder metallurgy market is undergoing a structural expansion, projected to reach $21.8 Billion by 2030 with a CAGR of 6.2%. The primary catalysts driving this growth are the global automotive transition toward electric vehicle (EV) multi-stage gearboxes, high-efficiency VVT/VPT timing systems, surgical robotic components, and lightweight consumer hardware.
China has established itself as the world's most comprehensive manufacturing ecosystem for sintered components and Metal Injection Molding (MIM). Localized industrial clusters in Ningbo and Zhejiang integrate powder atomization, precision mold tooling, high-pressure hydraulic pressing, and continuous vacuum debinding-sintering into a single continuous chain.
Process Technology Comparison: PM vs. MIM vs. CNC
Selecting the appropriate production route is essential for optimizing cost-per-part and mechanical performance. While conventional press-and-sinter Powder Metallurgy (PM) dominates high-volume 2.5D structural gears and oil pump rotors (up to 150mm diameter), Metal Injection Molding (MIM) excels at complex 3D micro-geometries under 100g.
Key Takeaway for Procurement Engineers
MIM and Sintered PM achieve 95% to 99% density compared to wrought steel, yielding 30% to 50% unit-cost reductions over 5-axis CNC milling by eliminating raw material scrap and secondary operations.
28,000m²
Production Facility
1,000 Ton
Compaction Press Capacity
±0.015mm
Sintered Tolerance Precision
48 Hours
Complete DFM Quote Turnaround
Supply Chain Architecture & Logistics
China Factory Supply Chain Resilience & Cost Leadership
How Ningbo Jiehuang Chiyang Electronic Tech Co., Ltd. leverages regional raw material integration, high-capacity tooling, and port access to guarantee zero-disruption delivery.
1. Raw Material Sourcing & Alloy Customization
Direct integration with domestic water/gas atomized powder producers and international suppliers (e.g., Höganäs) enables precise formulation of Fe-Ni, Fe-Cu-C, 17-4PH, 316L, and Titanium alloy powders. Pre-alloyed and diffusion-alloyed powders (Distaloy series) ensure homogeneous tensile strength and shrinkage predictability during sintering.
2. In-House Mold Design & Rapid Tooling Development
Equipped with slow-wire EDM, high-speed CNC engraving, and mirror-surface EDM, our tooling center produces multi-cavity press dies and MIM molds in 25–30 days. In-house tooling eliminates sub-contractor delays and maintains dimensional consistency across 1,000,000+ cycle production runs.
3. Ningbo Deep-Water Port & Export Infrastructure
Situated in Ningbo High-Tech Zone, less than 40 kilometers from Ningbo-Zhoushan Port (the world's largest container port by cargo throughput), JHMIM achieves seamless sea/air freight routing. Consolidated customs documentation and DDP shipping lower total landed costs for North American and European OEMs.
| Manufacturing Technology | Material Utilization % | Dimensional Tolerance | Surface Roughness (Ra) | Tooling Lead Time | Unit Cost (Volume >50k) |
|---|---|---|---|---|---|
| Powder Metallurgy (PM Press & Sinter) | 95% - 98% | ±0.015 mm - ±0.03 mm | 1.6 – 3.2 µm | 25 - 30 Days | Lowest |
| Metal Injection Molding (MIM) | 98% - 99% | ±0.03 mm - ±0.05 mm | 0.8 – 1.6 µm | 30 - 35 Days | Low to Medium |
| 5-Axis CNC Machining | 15% - 40% | ±0.005 mm | 0.4 – 0.8 µm | N/A (No Die) | Very High |
| Investment Casting (Lost Wax) | 60% - 75% | ±0.10 mm - ±0.20 mm | 3.2 – 6.3 µm | 40 - 50 Days | Medium to High |
Advanced Metallurgy Engineering
Technical Roadmap & Future Horizons
How next-generation sintering techniques, titanium MIM formulations, binder jetting integration, and micro-PM are pushing material boundaries.
Ultra-High Density Sintering (>7.55 g/cm³)
Implementation of high-temperature vacuum sintering (>1300°C) combined with warm compaction technology to eliminate interconnected porosity. Yields tensile strength exceeding 1200 MPa and impact toughness approaching forged alloys for heavy-duty EV gearboxes.
Titanium Metal Injection Molding (TiMIM) Innovation
Pioneering low-oxygen debinding protocols for Ti-6Al-4V and pure Titanium powders. Enables weight-critical, highly biocompatible components for surgical scalpel handles, orthopedics, and aerospace micro-fasteners.
Hybrid Additive Manufacturing & PM Integration
Combining metal 3D printing (Binder Jetting / DMLS) for rapid prototype validation with production powder metallurgy tooling. Shortens time-to-market by permitting functional testing prior to hard-tooling investment.
Micro-MIM & High-Aspect-Ratio Geometries
Engineering micro-components weighing as little as 0.02 grams with wall thicknesses down to 0.2mm for smartphone camera actuators, medical biopsy forceps, and micro-fluidic valve control assemblies.
Application Engineering Case Studies
Localized Industrial Application Scenarios & Commercial Deployments
Field-tested PM & MIM engineered solutions operating in demanding automotive, medical, power tool, and industrial environments worldwide.
Automotive Powertrains, VVT Components & Oil Pump Rotors
Modern internal combustion engines and hybrid vehicles demand precise oil flow and dynamic timing response. JHMIM mass-produces sintered trochoidal engine oil pump rotors and Variable Valve Timing (VVT) stator/rotor pairs. Using copper-steels (MPIF FC-0208) and heat-treated low-alloy steel (FLN2-4405), these parts withstand continuous hydraulic stress, reducing mechanical wear and optimizing fuel economy.
Medical Surgical Instruments & Endoscopic Jaws
Surgical devices require sub-millimeter intricate geometries combined with strict biocompatibility and corrosion resistance. Utilizing 17-4PH and 316L stainless steel via MIM processing, JHMIM manufactures endoscopic grasper jaws, surgical stapler housings, and scalpel handle locks. The resulting components feature mirror-polished finishes, high tensile strength (>1100 MPa), and pass rigorous passivation and autoclave tests.
Consumer Electronics: SIM Trays, Watch Clasps & Foldable Hinges
Smartphones, wearables, and foldable laptops demand ultra-thin structural brackets and tactile exterior hardware. MIM processing permits complex undercuts and micro-logos directly molded into stainless steel SIM card slots, smartwatch deployment buckles, and multi-axis hinge structures. PVD plating and mirror polishing yield premium cosmetic appeal alongside long-term mechanical durability.
Industrial Power Tools, Planetary Gearboxes & Pump Flanges
Professional power tools and hydraulic machinery demand gears that absorb peak torsional loads. JHMIM supplies high-density sintered spur gears, internal ring gears, planetary carrier assemblies, and water pump flanges. Induction hardening and steam treating enhance surface wear resistance to HRC 45–55, extending gear life under extreme duty cycles.
E-E-A-T Quality Commitment
Quality Engineering, Compliance & Localized Support
Rigorous multi-stage quality control systems, international regulatory compliance, and dedicated DFM engineering support for zero-defect global manufacturing.
ISO 9001 & IATF 16949 Certification Execution
Our manufacturing operations strictly conform to IATF 16949 (Automotive Quality Management Systems) and ISO 9001 standards. APQP (Advanced Product Quality Planning), PPAP Level 3 documentation, FMEA, and SPC statistical process controls are embedded into every production lot to ensure lot-to-lot repeatability.
Advanced Metrology Inspection Lab
Equipped with Zeiss 3D Coordinate Measuring Machines (CMM), Video Measurement Systems (OMM), optical emission spectrometers (OES), metallographic micro-structure analyzers, density balances, and digital hardness testers. Every batch undergoes 100% key dimension verification before shipment.
Global Regulatory Compliance & DFM Support
All raw powders and surface coatings comply with EU REACH, RoHS, and Conflict Minerals regulations. Our bilingual engineering support team provides preliminary Design for Manufacturability (DFM) feedback and complete quotation breakdowns within 48 hours under strict non-disclosure agreement (NDA) terms.
Complete Precision Catalog
Additional OEM Metallurgy & Die Casting Solutions
Explore custom gears, watch clasps, CNC machine chain drag links, plastic injection molds, and aluminum/zinc die casting hardware built to customer engineering drawings.

Wholesale OEM Manufacturer China CNC Machine Parts of Tz Type Black Cable Drag Chain Enhanced Type Manufacturers, Factory

China OEM Custom MIM Stainless Steel Watch Buckles Clasps Supplier, Suppliers

China Online Exporter China OEM Plastic Injection Molding Factory Plastic Molding Company Manufacturer, Suppliers
Wholesale China Factory for Stainless Steel Sintered Powder Metallurgy Parts MIM Metal Injection Molding Gear Part for Electronic Components Supplier, Factories
China China Customized Spur Gear Supplier Supplier, Factories

China Discount wholesale China Powder Metallurgy Customized Components Sintered Spare Parts Manufacturers, Suppliers

Wholesale Big Discount Factory OEM Custom China Aluminum Die Casting Service Manufacturer, Supplier

Wholesale OEM Customized Chinese Factory Precision Custom Hardware Accessories Magnesium Zinc Aluminum Parts Die Casting Supplier, Factories
Engineering Knowledge Base & FAQ
Frequently Asked Questions by Procurement Engineers
Direct technical answers regarding PM and MIM tolerances, material equivalencies, minimum order quantities, and tooling lead times.
What is the core difference between press-and-sinter Powder Metallurgy (PM) and Metal Injection Molding (MIM)?
Conventional PM utilizes uniaxial mechanical presses to compact dry metal powder into 2.5D shapes (such as gears, bushings, and oil pump rotors) with typical densities of 88–94%. MIM mixes fine atomized powder with a thermoplastic binder system to injection mold complex 3D shapes (similar to plastic molding), followed by debinding and sintering. MIM yields 96–99% theoretical density and supports undercuts, internal threads, and complex wall changes.
What dimensional tolerances can China Powder Metallurgy factories maintain during mass production?
Standard sintered tolerances range between ±0.03mm and ±0.05mm per inch. With secondary sizing (coining) or CNC finishing, critical features can be held to ±0.015mm. MIM components typically hold ±0.3% to ±0.5% of nominal dimensions as-sintered.
What are the Minimum Order Quantities (MOQ) and lead times for prototype tooling vs production tooling?
For MIM parts, standard production MOQ is 2,000 pieces. For PM press-and-sinter gears, MOQ is typically 5,000 pieces due to press setup times. Production tooling lead time requires 25 to 35 days, including sample inspection (FAI). Prototype verification can be accelerated via 3D metal printing (Binder Jetting) within 7 to 10 days.
How does Ningbo Jiehuang guarantee Intellectual Property (IP) security and NDA protection?
We routinely execute legally binding Non-Disclosure Agreements (NDAs) prior to receiving customer STEP/PDF files. All engineering drawings are managed under encrypted internal servers with restricted role-based access control.