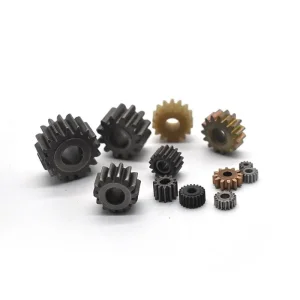
Featured Precision OEM Metal Components Showcase
Explore our core manufacturing outputs covering custom high-pressure die casting, MIM components, engine cylinder spares, and sintered filtration components engineered for high-rigor applications.






1. Global Industrial Landscape: The Evolving Dynamics of OEM Precision Manufacturing
The global manufacturing architecture is undergoing a structural paradigm shift. As Tier-1 global original equipment manufacturers (OEMs) demand tighter tolerances, reduced component weights, and streamlined total cost of ownership (TCO), selecting certified OEM Products Suppliers & Factories has escalated from a purely tactical purchasing task into a critical strategic enterprise decision.
Modern industrial ecosystems across North America, Western Europe, and Asia-Pacific require precision metal components capable of executing under extreme thermodynamic and mechanical strain. Whether for electric vehicle (EV) powertrains, medical-grade endoscopic instruments, defense-grade locking mechanisms, or smart wearable structural frames, the reliance on advanced metallurgy—spanning Metal Injection Molding (MIM), high-density Powder Metallurgy (PM), and high-pressure Aluminum/Zinc Die Casting—has become foundational.
In traditional subtractive manufacturing (such as multi-axis CNC milling), high material scrap rates (often exceeding 60-70% for complex internal geometries) inflate per-unit costs dramatically. Near-Net-Shape (NNS) manufacturing technologies supported by China’s premier OEM supplier networks optimize material yield to upwards of 95%, virtually eliminating raw material waste while ensuring high dynamic stress resistance and metallurgical uniformity.
2. Technical Roadmap: Selecting the Right Manufacturing Route
A primary challenge for procurement officers and senior DFM (Design for Manufacturability) engineers is determining the optimal manufacturing route for complex metallic components. Below is an engineering benchmark outlining performance, dimensional constraints, and operational sweet spots across core manufacturing processes.
| Manufacturing Technology | Primary Material Alloys | Part Weight Range | Dimensional Tolerance | Geometry Complexity | Economic MOQ |
|---|---|---|---|---|---|
| Metal Injection Molding (MIM) | 17-4PH, 316L, Ti-6Al-4V, Fe-Ni Alloys | 0.1g to 286g | ±0.3% to ±0.5% (±0.02mm) | Extreme (Undercuts, Micro-holes) | 2,000 Pcs |
| Powder Metallurgy (PM) | Fe-Cu, Sintered Steels, Bronze (MPIF 35) | 5g to 2,000g | ±0.05mm (Press-Direction) | Medium (2.5D Gear Profiles) | 5,000 Pcs |
| Aluminum High-Pressure Die Casting | ADC12, A380, AlSi10Mg | 20g to 15,000g | ±0.05mm to ±0.1mm | High (Thin-walled Housings) | 2,000 Pcs |
| Zinc Alloy Die Casting (Zamak 3/5) | Zamak #3, Zamak #5, ZA-8 | 5g to 3,000g | ±0.02mm to ±0.05mm | High (Cosmetic Hardware) | 3,000 Pcs |
| Multi-Axis CNC Machining | Aluminum, Stainless, Brass, Titanium | 1g to Unlimited | ±0.005mm (Ultra-Precision) | Tool-Path Constrained | 100 Pcs |
MIM Deep-Dive
Combining plastic injection molding geometric freedom with the mechanical strength of forged metal. Ideal for intricate parts under 100 grams requiring tensile strength above 1000 MPa after heat treatment.
High-Tonnage PM
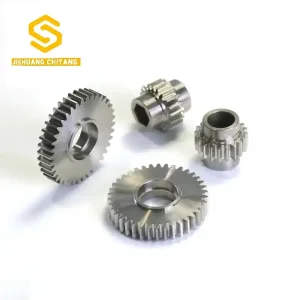
Utilizing 1,000-ton automated compaction presses to compact elemental metal powders into high-density gear sets, timing pulleys, and transmission hubs with exceptional wear resistance.
Aluminium Die Casting
High-speed molten metal injection under high hydraulic pressures. Delivers thin-walled, light-weight, highly conductive engine cylinders, electronic enclosures, and automotive housings.
3. China's OEM Manufacturing Hubs: Supply Chain Resilience & Cost Advantages
Global sourcing managers working with top China OEM suppliers like Ningbo Jiehuang Chiyang Electronic Tech Co., Ltd. (JHMIM) benefit from unmatched industrial concentration. Situated in Ningbo, Zhejiang Province—the epicenter of China's metallurgy, mold tooling, and port logistics ecosystem—our facilities reduce supply chain friction through hyper-localized integration.
Complete Ecosystem Proximity
From raw metal powder atomization suppliers and certified ingot refineries to specialized heat-treatment labs and surface coaters (PVD, Anodizing, Electropolishing), everything operates within a 50-kilometer radius. This eliminates weeks of transit delay during iterative prototyping phases.
In-House Tooling & Design
Equipped with high-speed CNC centers, wire EDM, and mirror-surface sinker EDM machinery, our mold tooling shop completes complex multi-cavity injection and casting molds within 25 to 35 business days—cutting traditional Western lead times by more than 50%.
Agile Manufacturing & Ramp-Up
Supported by state-of-the-art continuous atmosphere sintering furnaces (vacuum and hydrogen debinding continuous systems), our daily MIM production throughput exceeds hundreds of thousands of parts, maintaining delivery compliance even under sudden volume spikes.
4. Application Scenarios Across Key Global Sectors
Custom metal components produced by certified OEM factories fulfill mission-critical demands across diverse industrial sectors. Below are authentic engineering application models:
Automotive & Powertrains
Components: Variable Valve Timing (VVT) rotors, turbocharger vanes, electric vehicle steering gear locks, sensor housings.
Engineering Impact: IATF 16949 certified MIM 17-4PH and sintered powder metallurgy gears ensure dynamic fatigue resistance exceeding 10 million cycles under extreme temperature fluctuations (-40°C to +150°C).
Medical & Surgical Devices
Components: Laparoscopic surgical grasper jaws, endoscopic hinges, titanium scalpel handles, dental instrument components.
Engineering Impact: Utilizing TiMIM (Titanium MIM) and 316L stainless steel provides full biocompatibility, autoclave sterilizability, and intricate micro-geometries unachievable through conventional machining.
Consumer Smart Hardware
Components: Foldable smartphone screen hinges, smartwatch chassis, camera ring bezel guards, earphone structural brackets.
Engineering Impact: Ultra-thin wall MIM capabilities down to 0.3mm coupled with high-precision PVD physical vapor deposition coating deliver luxury-grade cosmetic aesthetics and rigid structural integrity.
Industrial Power Tools & Locks
Components: High-torque planetary gearboxes, hydraulic mini-valve cores, smart lock deadbolts, laser ceramic insulators.
Engineering Impact: High-density powder metallurgy gears sintered at 1280°C deliver extreme surface hardness (HRC 55-62 post-carburizing), reducing friction wear in high-load industrial power tools.
5. Quality Compliance, DFM Protocols & International Safeguards
To mitigate risk in cross-border manufacturing, top-tier OEM factories adhere to rigorous international quality control standards. Quality assurance starts far before physical production begins.
Free Engineer DFM Review
Every 2D (PDF) and 3D (STEP/IGES) file submitted undergoes computer-aided DFM flow simulation. Engineers analyze mold filling, shrinkage rates, gate location stress points, and wall thickness uniformity, providing a detailed DFM report within 24–48 hours.
Strict IP Protection & NDA
We protect client intellectual property with non-disclosure agreements (NDAs). All CAD designs, tool drawings, and project documentation remain stored on encrypted local servers with strict role-based authorization rules.
Metrology & Verification
Quality control centers feature ZEISS 3D Coordinate Measuring Machines (CMM), optical measuring projectors, X-ray fluorescence alloy analyzers (XRF), density meters, and digital hardness testers. FAI (First Article Inspection) and PPAP Level 3 reports are available.
6. Technical & Procurement Frequently Asked Questions (FAQ)
Find immediate answers to critical engineering, tooling, lead time, and commercial queries regarding custom OEM manufacturing.
Additional High-Precision Manufacturing Solutions
Explore our complete capabilities spanning micro gear manufacturing, specialized metal injection molding components, watch cases, and precision hardware locks.