
Explore our certified production line of ultra-high density sintered structural parts, MIM components, and precision die-cast alloys designed for global tier-1 automotive, medical, and industrial systems.
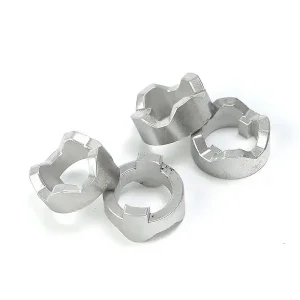





Understanding the technical transformation from legacy sub-tractive machining to advanced solid-state diffusion, powder compaction, and catalytic debinding sintering systems.
Shift Towards Near-Net-Shape Powder Metallurgy
The phrase "Sinter Metal Imalat San A Ş" (designating corporate sintering manufacturing entities within international supply networks) represents the epicenter of modern mechanical engineering. Global procurement leaders are rapidly abandoning multi-axis CNC subtractive milling in favor of Sintered Powder Metallurgy (PM) and Metal Injection Molding (MIM). Why? Because traditional machining wastes up to 60% of raw bar stock in scrap material, whereas powder metallurgy achieves a near-net-shape utilization rate exceeding 95%.
High-Density Sintering Furnace Operations
Modern China sinter metal factories operate atmosphere-controlled continuous belt furnaces and high-vacuum batch furnaces reaching temperatures of up to 1,380°C. By precisely controlling hydrogen, nitrogen, and argon gas shrouds, atomic diffusion occurs across metal powder boundaries without melting the base metal completely. This results in uniform grain refinement, tailored porosity, micro-structural integrity, and mechanical properties equivalent to wrought alloys.
Engineering Information Gain: Sintered stainless steel (316L, 17-4PH) and low-alloy steel components produced via MIM exhibit tensile strengths exceeding 1,150 MPa after specialized vacuum heat treatment (H900 condition), rendering them suitable for high-stress automotive valve trains and surgical articulation joints.
Key technological innovations driving the evolution of China sinter metal factories to meet stringent global aerospace, automotive, and medical specifications.
1. Catalytic & Solvent Debinding Advancements
The transition from slow thermal debinding to nitric-acid catalytic debinding has reduced binder-removal cycle times from 48 hours to under 6 hours. This process yields a clean "brown part" with zero carbon residue, ensuring carbon content compliance in sensitive alloys like 316L stainless steel.
2. Ultra-Fine Gas Atomized Powders
Leading Chinese factories now utilize micro-fine gas-atomized spherical powders ($D_{50} < 10\,\mu\text{m}$) rather than irregular water-atomized powders. This yields superior green density, smoother surface finishes ($Ra < 1.6\,\mu\text{m}$), and minimal post-sinter shrinkage variations.
3. Titanium MIM (TiMIM) Maturation
Once limited to aerospace prototyping, Ti-6Al-4V titanium metal injection molding is now mass-produced in China. Custom vacuum argon furnaces control interstitial oxygen pickup to under 0.15 wt%, delivering biocompatible lightweight components for medical implants and premium electronics.
Why multinational buyers require more than just low unit prices: The critical evaluation framework for selecting a Chinese sintering partner.
What Global Purchasing Directors Demand:
- Strict Metallurgical Consistency: Lot-to-lot alloy chemistry balance verified via optical emission spectrometers (OES) and ICP-MS testing.
- Early DFM (Design for Manufacturability) Engagement: Engineering assistance to redesign heavy machined blocks into thin-walled, rib-reinforced sintered parts with optimal mold draft angles (0.5° to 1°).
- Total Cost of Ownership (TCO) Transparency: Clear breakdown of tooling amortization (hardened H13 steel molds rated for >1,000,000 shots), debinding consumables, and sintering energy overheads.
- Automated Secondary Processing: Integrated secondary operations including CNC coining, magnetic polishing, vacuum oil impregnation, and PVD physical vapor deposition coating.
Procurement Risk Mitigation Matrix
How Ningbo Jiehuang (JHMIM) mitigates traditional cross-border manufacturing vulnerabilities:
Leveraging Ningbo's world-class industrial cluster, automated robotic cell molding, and digital twin monitoring to compress production cycles by 40%.
Complete Regional Ecosystem
Located in Ningbo, Zhejiang Province, our facility sits at the core of the world's most concentrated precision metal supply chain. Powder suppliers, mold toolmakers, vacuum furnace technicians, and electroplating facilities are within a 30-minute radius, eliminating logistic bottlenecks.
MES Digital Process Tracking
Every batch of raw metal powder is assigned a unique digital barcode. Our Manufacturing Execution System (MES) records feedstock mixing ratios, injection pressure curves, debinding fluid temperatures, and sintering vacuum levels for complete 100% trace-ability.
Rapid Tooling & Prototyping
Before cutting production molds from hardened H13/S136 steel, we utilize Selective Laser Melting (SLM) metal 3D printing to create functional prototype parts within 72 hours. Designers can validate mechanical fit before committing to full production tooling.
Objective engineering evaluation to guide your manufacturing process selection based on geometry, volume, material choices, and unit economics.
| Manufacturing Process | Suitable Geometries | Material Options | Relative Density | Dimensional Tolerance | Ideal Economic Order Quantity |
|---|---|---|---|---|---|
| Metal Injection Molding (MIM) | Ultra-complex 3D shapes, undercuts, internal threads, wall thickness 0.5–5.0 mm | Stainless Steels (316L, 17-4PH), Fe-Ni, Titanium, Tool Steels | 95% – 99% | ±0.3% to ±0.5% (±0.02 mm with sizing) | >2,000 pcs (High Volume) |
| Powder Metallurgy (PM Pressing) | 2.5D stepped gears, bushings, pulleys, symmetrical structural parts | Iron-Copper, Sintered Steels, Bronze, Stainless Steel | 85% – 92% (Oil impregnated option) | ±0.05 mm (ISO 2768-m) | >5,000 pcs (Mass Production) |
| Aluminum & Zinc Die Casting | Medium-to-large thin-walled housings, enclosures, heat sinks | A380, ADC12 Aluminum, Zamak 3/5 Zinc Alloys | 90% – 95% (Porosity near core) | ±0.10 mm | >2,000 pcs |
| Multi-Axis CNC Machining | Prismatic blocks, low-complexity rotational shafts, prototype plates | All Metals (Aluminum, Brass, Steel, Inconel, Titanium) | 100% (Wrought material) | ±0.005 mm to ±0.01 mm | 1 to 500 pcs (Low Volume) |
| SLM Metal 3D Printing | Organic topology-optimized lattices, conformal cooling channels | 316L, Ti-6Al-4V, Inconel 718, AlSi10Mg | >99.5% | ±0.10 mm | 1 to 50 pcs (Rapid Prototypes) |
Discover how custom sintered metal parts are integrated into mission-critical hardware across four prime industrial sectors.
Automotive Powertrain & Actuators
Sintered metal components excel in high-torque, oil-immersed automotive environments. We mass-produce Variable Valve Timing (VVT) rotors, oil pump gears, transmission synchronizer rings, and turbocharger wastegate levers. By utilizing alloy powder formulations like Fe-Cu-C and MIM 17-4PH, these parts endure over 300,000 km of continuous automotive operation without fatigue failure.
Medical Surgical Endocutters & Tools
Precision endoscopic surgical instruments demand sub-millimeter intricate geometries with high mechanical strength. Through MIM 316L and TiMIM titanium injection molding, we manufacture surgical stapler jaws, laparoscopic grasper articulation hinges, and scalpels. Surface passivation ensures compliance with ISO 10993 cytotoxicity and biocompatibility standards.
Consumer Electronics & Smart Wearables
Smartphones, foldable displays, and smartwatches utilize ultra-compact metal mechanisms. Our micro-MIM capabilities produce foldable phone screen hinges, smartwatch chassis brackets, camera ring frames, and earphone audio acoustic chambers. Complex thin-walled structures down to 0.4 mm are achieved with pristine mirror-polished finishes.
Industrial Lock Hardware & Power Tools
High-security anti-theft lock cylinders, padlock cores, and planetary gearboxes for cordless power drills require extreme surface hardness and wear resistance. Sinter-hardening processes combine sintering and rapid gas quenching, yielding surface hardness up to 45-55 HRC without secondary heat treatment distortion.
Our Ningbo manufacturing facility operates under audited IATF 16949 and ISO 9001 quality control frameworks to guarantee zero-defect delivery.
1. Raw Material Verification
Every incoming batch of metal powder undergoes laser diffraction particle size distribution analysis ($D_{10}, D_{50}, D_{90}$), hall flow meter speed testing, and apparent density measurement to ensure injection stability.
2. CMM & Optical Metrology
In-house inspection labs house Zeiss 3D Coordinate Measuring Machines (CMM), keyence optical image measuring systems, and roughness testers capable of verifying complex gear pitch circle diameters to $\pm 0.005\,\text{mm}$.
3. Metallurgical & Density Checks
Achieved density is verified using the Archimedes water displacement principle (ISO 3369). Cross-sectional samples are mounted, polished, and micro-etched for photomicrographic grain boundary and micro-hardness profile analysis (Vickers/Rockwell).
Clear answers to technical inquiries surrounding MIM, powder metallurgy, DFM reviews, lead times, and customization capabilities.
Discover more specialized hardware, custom die castings, engine aftermarket components, and sintered mechanical joint elements.






Ready to Optimize Your Metal Components Sourcing?
Upload your 2D/3D technical drawings today. Our senior metallurgical engineers will conduct a thorough DFM review and return an actionable quotation within 48 hours.