
Precision OEM Metal & Gear Components (Catalog Selection Part 1)
Explore our foundational range of powder metallurgy components, sintered gears, MIM surgical hardware, and precision die-cast enclosures tailored for global industrial supply chains.


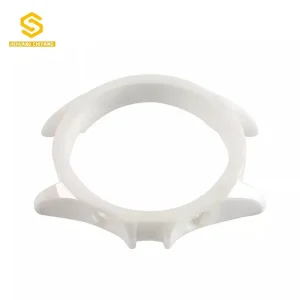




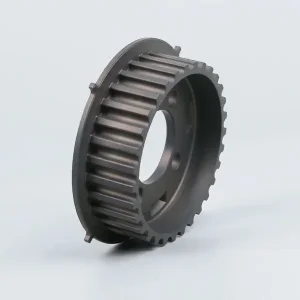
Technical Whitepaper: Engineering Next-Gen Precision Gearing in China
In modern mechanical power transmission, gears serve as the fundamental backbone for motion control, torque conversion, and positional accuracy. As global industries shift toward electric vehicles (EVs), surgical robotics, high-torque industrial automation, and micro-electromechanical systems (MEMS), the demand for high-strength, complex-geometry gears has expanded beyond traditional gear hobbing and shaping methods.
As a premiere China gear manufacturer, Ningbo Jiehuang Chiyang Electronic Tech Co., Ltd. (JHMIM) bridges advanced material science with high-volume manufacturing technologies. By leveraging Metal Injection Molding (MIM) and Powder Metallurgy (PM) alongside high-tonnage aluminum/zinc pressure die casting, we deliver near-net-shape gearing solutions that drastically minimize material waste, eliminate multi-axis machining passes, and achieve AGMA Quality Class 8 to 11 tolerances right out of the sintering furnace.
1. Macro-Industrial Trends & Global Gear Supply Chain Realities
The global precision gear market faces dual pressures: rising raw material expenditures (such as specialty alloy nickel, cobalt, and molybdenum steels) and stringent noise, vibration, and harshness (NVH) compliance standards. Traditional subtractive manufacturing (CNC milling, gear shaping, gear hobbing) suffers from material loss rates up to 60–70% when creating complex gear clusters, internal spline profiles, double-helical teeth, or integrated planetary carriers.
Partnering with a specialized Chinese wholesale manufacturer provides global original equipment manufacturers (OEMs) with strategic structural advantages:
- Integrated Material Synthesis: In-house powder blending allows custom alloy tailing (e.g., Fe-Ni-Cu-Mo structural steels, stainless steel 17-4PH, 316L, and Titanium TiMIM alloys) tuned for specific yield strengths, elongation limits, and magnetic permeability.
- Capital Efficiency & Scale: High-speed hydraulic compaction presses (up to 1,000 tons / 10,000 kN) and continuous atmosphere-controlled sintering furnaces permit monthly volume outputs in the millions of pieces with negligible unit-to-unit variance.
- Structural Weight & Energy Reduction: Near-net-shape forming enables integrated lightweighting pockets, hollow shafts, and optimized tooth root fillet profiles that cannot be physically accessed by conventional cutting tools.
2. Metallurgy Science: Sintering Kinetics & Powder Densification
The strength of a powder metallurgy gear is inextricably tied to its final sintered density and microstructural phase distribution. Sintering involves heating compacted metal powder green bodies below their primary melting temperature in a protective reducing atmosphere (e.g., dissociated ammonia, synthetic endothermic gas, or high-vacuum argon environment).
Solid-State Diffusion
Atomic migration across powder contact boundaries eliminates micro-voids, transforming mechanical powder mechanical locks into high-integrity metallic atomic bonds.
Liquid Phase Sintering
By introducing transient low-melting phase elements (such as copper or phosphorus additives), liquid capillary action draws particles together, accelerating density up to 7.4 - 7.6 g/cm³.
Surface Hardening Kinetics
Post-sintering carbonitriding or induction hardening establishes ultra-hard wear surfaces (58-62 HRC) while preserving a resilient ductile core for shock-load damping.
3. Process Evaluation: MIM vs. PM vs. Die-Casting vs. CNC Machining
Selecting the optimal manufacturing route depends on gear geometry, module size, annual volume, and torque load requirements. The matrix below outlines how Jiehuang's core engineering processes compare against traditional CNC gear cutting:
| Process Technology | Optimal Geometry / Modules | Density Range | AGMA Precision Class | Economic MOQ | Material Efficiency |
|---|---|---|---|---|---|
| Metal Injection Molding (MIM) | Micro gears, complex clusters, complex 3D features (m < 0.5 to 2.0 mm) | 7.5 - 7.8 g/cm³ (>97%) | AGMA 8 - 10 | 2,000 pcs | 95% - 98% (Near Zero Waste) |
| Powder Metallurgy (PM Pressing) | Spur gears, helical gears, timing pulleys (m > 0.8 mm up to 150mm dia) | 6.8 - 7.4 g/cm³ (90-95%) | AGMA 7 - 9 | 5,000 pcs | 92% - 96% |
| Zinc & Aluminum Die Casting | Lightweight non-structural gearing, actuator housings, low-torque drives | Cast Density (~2.7 - 6.6 g/cm³) | AGMA 6 - 8 | 2,000 pcs | 85% - 90% (Scrap Recyclable) |
| Subtractive CNC Hobbing | Simple profile shafts, prototyping, thick spur gears | Wrought Density (100%) | AGMA 10 - 12 | 1 - 500 pcs | 30% - 50% (High Scrap Rate) |
Localized Industry Application Scenarios
JHMIM supplies precision-engineered metal gears and custom components to OEM Tier-1 and Tier-2 manufacturers across North America, Europe, Japan, and Southeast Asia. Discover how our custom gearing technologies power mission-critical equipment globally.
Automotive Powertrain & Actuators
Sintered steel electronic throttle body (ETB) gears, Variable Valve Timing (VVT) rotors, seat recliner gears, and electric parking brake (EPB) planetary gearboxes engineered under IATF 16949 oversight.
Medical Surgical Robotics
Micro titanium (TiMIM) and 316L stainless steel gearing for endoscopic staplers, robotic arm wrist joints, and peristaltic pump drives demanding extreme biocompatibility and sterilisability.
High-Torque Power Tools
Heavy-duty powdered metal bevel gears, impact driver hammers, and sun gears utilizing high-density Fe-Ni alloys (MPIF FN-0205) capable of enduring sudden torsional shock loads up to 150 Nm.
Smart Consumer Devices
Ultra-quiet micro gearboxes for smart door locks, drone gimbal positioners, camera zoom modules, and wearable wrist accessories requiring fine pitch modules down to m = 0.15 mm.
Institutional Quality Assurance & DFM Protocols
Achieving consistent tooth profile geometry, minimal lead error, and controlled pitch variation across millions of production units requires rigorous process control. At Jiehuang, every drawing undergoes comprehensive Design for Manufacturability (DFM) verification prior to mold tooling creation.
Involute Profile & Lead Error Testing
Automated gear measurement centers evaluate pitch deviation (Fp), profile error (ffa), and total composite error (Fi) against ISO 1328 and AGMA 2015 standards.
X-Ray Micro-CT & Density Mapping
Non-destructive internal void detection confirms 100% solid core integrity in high-load planetary gears and high-stress automotive safety parts.
Full Batch Material Traceability
Every shipment includes chemical spectral analysis reports, hardness test certificates (Vickers/Rockwell), and full CMM dimension data.
The JHMIM Compliance Guarantee
Navigating global trade mandates requires complete transparency and zero defect rates. We support our international partners with complete regulatory documentation:
- IATF 16949 Automotive Quality Management
- ISO 9001:2015 Certified Production Line
- RoHS, REACH, and Conflict Minerals Declaration
- Strict Non-Disclosure Agreements (NDA) Protection
- Dual-Sourcing & Supply Chain Contingency Frameworks
Technology Roadmap & Future Engineering Outlook (2026–2035)
As automated assembly and electrification drive tighter performance criteria, Jiehuang continues to pioneer advancements in powder metallurgy and micro-molding processes.
Warm Compaction & Surface Rolling
Integrating heated powder press dies with post-sinter gear tooth rolling to achieve surface densities exceeding 7.75 g/cm³, matching wrought alloy performance for heavy-duty EV gearboxes.
3D Printing + MIM Tooling Twins
Combining direct metal laser sintering (DMLS) rapid prototyping with digital twin simulation software to refine thermal shrink factors before cutting hard steel injection molds.
Zero-Magnetic Micro-Gears
Developing high-strength zirconia ceramic (CIM) and titanium alloy micro-gears for high-field MRI environments, aerospace sensors, and extreme chemical immersion pumps.
Precision OEM Metal & Gear Components (Catalog Selection Part 2)
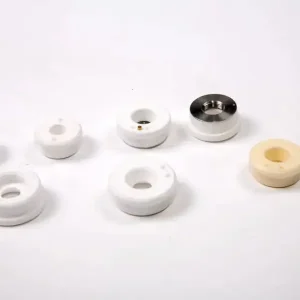
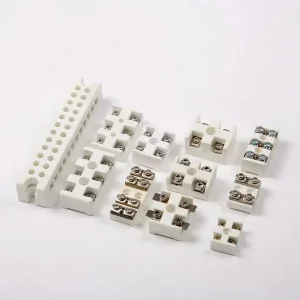
Explore our specialized range of sintered bushings, copper-based structural parts, ceramic connectors, and automotive gear castings tailored for high-volume OEM supply chains.





Frequently Asked Questions (Technical & Procurement FAQ)
Get answers to common engineering, process selection, and logistics questions directly from our senior metallurgy team.
MIM allows for the mass production of highly complex, 3D gear geometries (such as integrated dual gears, internal splines, and micro gears under 100 grams) in a single operation. While CNC hobbing requires multiple setups and wastes up to 60% of raw bar stock, MIM produces near-net-shape components with 95%+ material utilization, saving 30% to 50% on total part cost at volumes over 2,000 units.
Out of the sintering furnace, our powder metallurgy and MIM gears reliably achieve AGMA Quality Class 8 to 9 (ISO 1328 Class 8-9). By adding secondary precision sizing, re-pressing, or gear tooth shaving, we can achieve AGMA Class 10 to 11 for high-precision automotive and medical applications.
Yes. We utilize in-house Direct Metal Laser Sintering (DMLS) 3D printing equipment to produce functional metal prototypes within 5-7 business days. This allows engineers to verify gear tooth mesh, backlash, and mechanical fit prior to committing to hard injection mold tooling.
We process a broad matrix of materials including Stainless Steels (17-4PH, 316L, 440C), Low-Alloy Steels (MPIF FN-0205, FN-0208, FL-4405 for high impact strength), Copper-Infiltrated Steels (FX-2008), Titanium Alloys (Ti-6Al-4V via TiMIM), and Engineering Ceramics (Zirconia/Alumina via CIM).
Standard mold tooling and initial sample inspection reports (ISIR/PPAP Level 3) are completed in approximately 25 to 35 days. Mass production lead times are typically 3 to 4 weeks depending on batch volume and secondary finishing treatments.
We execute legally binding bilateral NDAs before reviewing any engineering CAD files or drawings. All client data is encrypted and housed on isolated internal servers with strictly controlled staff access rights.
Our economic MOQ is 2,000 pieces for MIM parts, 5,000 pieces for standard powder metallurgy gear pressings, and 2,000 pieces for aluminum/zinc die-cast enclosures. Pilot batch runs for high-value automotive or medical components can be evaluated individually.
We deliver under all international commercial terms (FOB Ningbo/Shanghai, CIF, DDP, DAP). Our logistics team manages export customs clearance, tariff classification documentation, and air/sea freight forwarding to your factory door.
Ready to Optimize Your Gear Manufacturing Costs?
Send us your 2D (PDF) and 3D (STEP/IGES) CAD drawings today. Receive a comprehensive DFM review and formal unit price quotation within 48 hours.