
High-Precision OEM Powder Metallurgy Parts
Explore our core sintered metal, MIM lock/gear components, and custom die-casting products certified under IATF 16949 standards.






The Technical Evolution of Powder Metallurgy (PM) in Motorcycle Manufacturing
In modern powersports, automotive engineering, and electric motorcycle (e-motorcycle) design, Powder Metallurgy (PM) and Metal Injection Molding (MIM) have emerged as critical manufacturing technologies. Replacing traditional subtractive CNC machining and drop-forging, PM technology delivers superior material utilization (up to 95%), complex near-net-shape geometries, and unmatched cost-efficiency at high production volumes.
High Torque & Fatigue Strength
Automotive-grade PM gears utilize Fe-Ni-Mo alloy steel powders, engineered to withstand intense rotational stress, high-impact engine combustion strokes, and continuous multi-speed transmission torque transfer.
Complex Near-Net Geometries
Eliminate costly secondary milling. Sintered parts effortlessly integrate helical gear teeth, internal splines, oil passages, and mounting flanges directly into the primary compaction die cycle.
Self-Lubrication Properties
Controlled micro-porosity impregnation with synthetic lubricants allows PM oil-impregnated bronze and iron bearings to achieve low friction coefficients and zero maintenance in engine valvetrains.
Global Commercial Landscape & Application Scenarios of PM Motorcycle Components
The global motorcycle market—spanning internal combustion engine (ICE) commuting bikes, high-displacement racing motorcycles, heavy-duty cruisers, and rapidly expanding electric motorbikes—demands components that balance weight reduction with structural reliability.
1. Engine & Powertrain Assemblies
Motorcycle combustion engines require high-precision components capable of continuous operation at speeds up to 14,000 RPM under elevated thermal conditions. Powder metallurgy delivers specialized alloys tailored for engine efficiency:
- Camshaft Valve Timing Sprockets: Produced via sinter-hardening, offering wear-resistant teeth profiles without requiring post-heat-treatment distortion rectification.
- Oil Pump Rotors (Gerotors): Sintered iron-nickel inner and outer rotors providing tight trochoidal tolerances for maximum hydraulic fluid delivery pressure.
- Valve Guides & Valve Seats: Engineered with copper-infiltrated iron alloys for rapid heat dissipation away from cylinder heads.
- Starter Motor Drive Pinions: High-impact PM steel pinions designed to withstand high engagement torque spikes during ignition.
2. Transmission & Gearbox Modules
Manual and automatic motorcycle transmissions rely on sintered gears for smooth gear engagement, reduced gear whine, and durability under rapid shifting loads:
- Synchronizer Hubs & Shift Forks: Net-shape MIM stainless steel and low-alloy PM components featuring intricate internal grooves and shift dogs.
- Sector Gears & Ratchet Dogs: Hardened iron-carbon PM parts providing high contact fatigue resistance for smooth shifting mechanisms.
- Clutch Hubs & Pressure Plates: Multi-spline aluminum alloy die-cast or sintered steel hubs reducing rotational inertia and clutch chatter.
3. Chassis, Braking & Safety Components
Modern motorcycles demand active safety integration, lightweight suspension components, and high-strength chassis hardware:
- ABS Pulser & Sensor Rings: Sintered magnetic stainless steel (SS 430L) rings providing high magnetic permeability for anti-lock braking systems.
- Shock Absorber Piston Rod Guides: Self-lubricating sintered bronze/iron bushings for hydraulic damping smoothness.
- Footrest Mounts & Handlebar Brackets: High-density die-cast aluminum or sintered alloy steel mounts resistant to dynamic fatigue.
4. Next-Gen Electric Motorcycle (E-Mobility) Drives
The global transition toward electric two-wheelers (E2W) introduces unique requirements for electromagnetic performance and ultra-compact powertrains:
- Soft Magnetic Composite (SMC) Stators: Insulated iron powder compacts enabling 3D flux pathways for high-efficiency hub motors.
- Planetary Gear Reducers: High-density PM planetary gear sets engineered for high-RPM electric motors requiring whisper-quiet operation.
Why Global Tier-1 OEMs Partner with China PM Manufacturers
China, particularly the Ningbo and Yangtze River Delta industrial clusters, has established itself as the global epicenter for precision powder metallurgy, MIM technology, and mold design. By pairing automated manufacturing with sophisticated metallurgy R&D, Chinese manufacturers offer global buyers distinct competitive leverage.
In-House Tooling & Rapid DFM
Equipped with high-speed CNC milling, wire-EDM, and 3D metal printing prototype capability, custom compacting tool steel dies (D2, M2, Tungsten Carbide) are fabricated in as fast as 20 to 30 days, slashing NPI (New Product Introduction) cycles.
1,000-Ton Automated Compacting Presses
Utilizing multi-level CNC hydraulic compaction presses ranging from 15 tons up to 1,000 tons (10,000 kN), ensuring uniform green density distribution across complex stepped gears and multi-level structural parts.
IATF 16949 Quality Management
Rigorous quality controls including CMM 3D dimensional verification, gear tooth profile checking, density testing (Archimedes method), metallographic analysis, and 100% key dimension optical sorting.
Powder Metallurgy & MIM Material Performance Matrix
Selecting the correct material standard (MPIF 35, DIN 3990, JIS Z2550) is vital for ensuring component performance under severe fatigue and wear environments. The table below outlines key engineering alloys utilized in PM motorcycle part fabrication.
| Material Standard | Composition Alloy | Sintered Density (g/cm³) | Tensile Strength (MPa) | Hardness (HRC/HRB) | Target Motorcycle Application |
|---|---|---|---|---|---|
| MPIF FN-0205-80HT | Fe-2.0Ni-0.5C (Heat Treated) | 7.20 - 7.45 | 850 - 1050 MPa | 35 - 45 HRC | Engine Transmission Gears, Timing Sprockets |
| MPIF FLN2-4405 | Fe-1.5Ni-0.8Mo-0.5C (Sinter Hardened) | 7.30 - 7.55 | 900 - 1150 MPa | 38 - 48 HRC | Heavy-Duty Starter Pinions, High-Torque Ratchets |
| MPIF FC-0208-50 | Fe-2.0Cu-0.8C (Copper Steel) | 6.80 - 7.15 | 450 - 650 MPa | 75 - 85 HRB | Structural Brackets, Oil Pump Outer Rotors |
| MIM SS-316L / 17-4PH | Stainless Steel (Injection Molded) | 7.60 - 7.80 | 900 - 1180 MPa | 36 - 42 HRC | ABS Sensor Rings, Shift Lock Dogs, Decorative Trim |
| MPIF CT-1000-K26 | Bronze (Sintered Self-Lubricating) | 6.40 - 6.80 | 180 - 240 MPa | 45 - 55 HRB | Valve Stem Bushings, Shock Absorber Bearings |
Key Technological Trends Shaping the Future of PM Motorcycle Parts
1. Surface Rolling & Densification
Localizing high pressure on gear tooth flanks via post-sinter rolling increases surface density close to theoretical solid steel (7.8 g/cm³), dramatically boosting bending strength for high-horsepower racing engines.
2. Sinter-Hardening Technology
By accelerating cooling rates directly inside high-temperature continuous atmosphere sintering furnaces, continuous martensitic transformation occurs, eliminating the distortion caused by separate oil quenching.
3. Titanium MIM (TiMIM) & Lightweighting
Adopting titanium alloy powder injection molding (Ti-6Al-4V) enables ultra-lightweight engine retainers, levers, and footpegs that offer 45% weight savings over steel while delivering extreme corrosion resistance.
Global OEM Procurement Checklist for Sourcing PM Motorcycle Parts
When evaluating wholesale PM motorcycle part suppliers and OEM manufacturers, procurement directors must verify engineering capability, quality systems, and supply resilience to eliminate risk.
1. Engineering & DFM Feasibility
Ensure your manufacturing partner conducts thorough Design for Manufacturability (DFM) reviews. Critical checks include verifying ejection draft angles (typically 0.5°–1°), avoiding ultra-thin tool ribs (< 0.8mm), and optimizing die press fill ratios to prevent density gradients.
2. Secondary Machining & Surface Operations
While PM achieves near-net shapes, high-precision features like transverse cross-holes, undercut grooves, or tight-tolerance bore fits (IT6 grade) require secondary CNC finishing, heat treating (carburizing, nitriding), and mechanical tumbling/anodizing.
3. Total Cost of Ownership (TCO) & Tooling ROI
Calculate amortization over expected production lifecycles. Compacting tooling costs are typically amortized within 10,000 to 50,000 units. For high-volume motorcycle models (100k+ units/year), PM tooling yields unit price reductions up to 60% compared to fully CNC-machined billets.
4. Traceability & Intellectual Property Security
Confirm the supplier operates under strict Non-Disclosure Agreements (NDAs), maintains batch-level raw powder lot traceability (spectrometer verification), and provides Full Initial Sample Inspection Reports (ISIR / PPAP Level 3).
Custom Engine Rotors, MIM Hardware & Sintered Assemblies
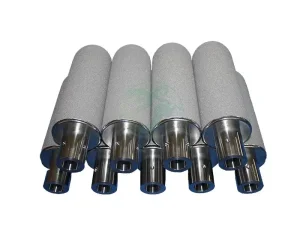
Browse additional specialized PM components, sintered filter elements, and custom metal powder components.





Technical & Commercial FAQ for Buyers
Answers to common engineering, procurement, and quality control questions regarding wholesale powder metallurgy motorcycle parts.