
Explore our custom manufacturing solutions spanning aluminum die casting, metal injection molding (MIM), and sintered powder metallurgy hardware.






The global powder metallurgy (PM) market is experiencing a profound transformation. Driven by structural shifts in global manufacturing toward near-net-shape processing, material efficiency, and green supply chains, PM technologies—including conventional press-and-sinter powder metal and advanced Metal Injection Molding (MIM)—have become foundational to modern industrial design.
Projected global powder metallurgy market size driven by automotive electrification, aerospace, and medical device manufacturing growth (2024–2032).
Near-net-shape manufacturing eliminates subtractive metal waste, drastically reducing raw material consumption compared to conventional CNC milling.
Achieved in high-volume production cycles by eliminating secondary machining, gear hobbing, and multi-part assembly steps.
Achieving wrought-like mechanical properties requires rigorous thermodynamic control, atomized powder selection, and precise solid-state sintering. As a tier-1 OEM factory partner, our operations strictly comply with MPIF Standard 35, ISO 9001, and IATF 16949 quality protocols.
Conventional powder metallurgy relies on high-tonnage compaction presses (ranging from 50 to 1,000+ tons) to force metal powders into carbide dies. The resulting "green body" achieves precise initial geometry before undergoing continuous belt atmosphere sintering at temperatures up to 1150°C–1280°C.
- Green Density Optimization: Uniform compaction pressure minimizes density gradients across complex gear teeth.
- Sinter-Hardening Technology: Rapid cooling within the sintering furnace converts austenite directly into martensite, eliminating secondary quenching steps.
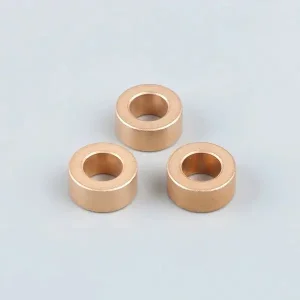
- Alloy Families: Iron-copper (FC-0208), Nickel-steel (FN-0205), Pre-alloyed molybdenum steels, and Sintered Bronze bearings.
Metal Injection Molding combines the geometric freedom of plastic injection molding with the structural integrity of high-performance metallic alloys. Fine spherical metal powders (typically 4–20 microns) are blended with a thermoplastic binder system to form feedstock.
- Debinding Process: Solvent immersion followed by thermal decomposition removes binder systems without disturbing delicate part geometries.
- High-Temperature Vacuum Sintering: Sintering at 1350°C–1380°C yields component densities exceeding 96% to 99% of theoretical limits.
- Alloy Families: Stainless Steels (316L, 17-4PH), Low Alloy Steels (4140, 8620), Titanium Alloys (Ti-6Al-4V), and Tungsten Heavy Alloys.
| Material Specification | Process Route | Sintered Density (g/cm³) | Tensile Strength (MPa) | Yield Strength (MPa) | Elongation (%) | Primary Industrial Application |
|---|---|---|---|---|---|---|
| MPIF FC-0208-60 | Press & Sinter | 6.8 - 7.2 | 450 - 620 | 380 - 480 | < 1.5% | High-torque timing gears, structural sprockets |
| MPIF FN-0205-180T | Sinter-Hardened | 7.0 - 7.4 | 850 - 1100 | 750 - 950 | < 0.5% | Automotive transmission planetary gears, oil pump rotors |
| MIM 17-4PH (H900) | Metal Injection Molding | 7.5 - 7.7 | 1150 - 1300 | 1050 - 1180 | 5.0 - 8.0% | Surgical jaw instruments, aerospace latch mechanisms |
| MIM 316L (As-Sintered) | Metal Injection Molding | 7.6 - 7.9 | 520 - 600 | 220 - 280 | 40.0 - 50.0% | Medical implants, consumer electronic watch cases |
| Sintered Bronze (SAE 841) | Oil-Impregnated PM | 6.4 - 6.8 | 130 - 180 | 90 - 120 | 9.0 - 12.0% | Self-lubricating sleeve bearings, motor bushings |
Our powder metallurgy components provide optimized physical performance across critical industrial sectors worldwide. Below are specialized localized integration scenarios where powder metal replaces high-cost machining or weak die-cast parts.
High-density sintered gears, variable valve timing (VVT) rotors, electronic parking brake (EPB) gearboxes, and electric drive pump components. Engineered for superior fatigue limits, acoustic damping (NVH reduction), and ultra-precise tooth profiles.
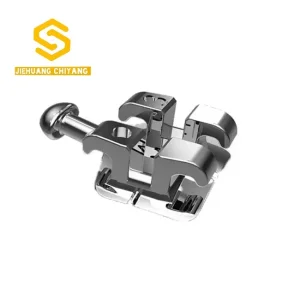
Biocompatible 316L and 17-4PH stainless steel MIM components for endoscopic surgical staplers, robotic arm wrist joints, dental orthodontic brackets, and scalpels. Provides 100% complex spatial geometry with zero micro-burrs.
Miniature MIM watch cases, smart-ring internal chassis, foldable smartphone screen hinges, and earphone acoustic driver housings. Achieves mirror-polish PVD decorative coatings and exceptionally high structural yield strength.
Heavily loaded planetary reduction gear sets, impact wrench anvils, fluid control valve plates, and hydraulic pump gerotors manufactured from heat-treated sinter-hardened alloy steels.
Titanium alloy (Ti-6Al-4V) MIM fasteners, drone engine throttle linkages, and high-density tungsten counterweights engineered to withstand severe thermal expansion and vibration loads.
High-security lock cylinders, mortise latch cams, clutch mechanism hubs, and biometric digital lock drive levers sintered with anti-drill copper-infiltrated steel alloys.
Choosing the right manufacturing process dictates total landed part costs, mechanical integrity, and time-to-market. Use our engineering decision baseline to evaluate trade-offs before tooling investment.
| Engineering Parameter | Press & Sinter PM | Metal Injection Molding (MIM) | High Pressure Die Casting | 5-Axis CNC Machining |
|---|---|---|---|---|
| Optimal Part Weight | 10g to 2.5 kg | 0.1g to 250g | 50g to 15 kg | Unlimited |
| Geometric Complexity | Moderate (2.5D shapes, press direction) | Maximum (Complex 3D geometries, undercuts) | High (Thin walls, deep cavities) | High (Constrained by tool access) |
| Dimensional Tolerance | ±0.05 mm (IT 8-9) | ±0.3% to ±0.5% | ±0.1 mm | ±0.005 mm (IT 5-6) |
| Material Efficiency | 95% - 98% | 95% - 98% | 85% - 90% | 15% - 40% (60%+ Scrap) |
| Surface Finish (Ra) | 1.6 – 3.2 µm | 0.8 – 1.6 µm | 1.2 – 3.2 µm | 0.4 – 1.6 µm |
| Break-Even Production Volume | 5,000+ units / year | 2,000+ units / year | 2,000+ units / year | 1 to 500 units |
As industrial automation, artificial intelligence, and carbon-neutral targets reshape global supply chains, our factory is advancing next-generation powder metallurgy innovations.
By blending binder jetting 3D printing (BJAM) directly with continuous belt furnace sintering, we eliminate physical mold tooling for pilot runs. This hybrid pathway reduces new product development cycles from 8 weeks to just 5 days while using identical MIM alloy chemistries.
Thermomechanical simulation software predicts part shrinkage, thermal gravity sagging, and furnace atmosphere carbon movement in advance. By pre-compensating tooling dimensions at the CAD stage, we achieve zero-defect first-article inspection (FAI) samples.
Commercialization of soft magnetic composites (SMCs) insulated with nano-dielectric coatings allows ultra-low hysteresis loss at high operating frequencies—setting a new benchmark for high-efficiency electric vehicle motor stators.
Implementing 100% green hydrogen debinding atmosphere gas systems and argon gas atomization powered by solar arrays reduces the carbon footprint per kilogram of finished sintered component by up to 68%.
Common technical and commercial questions answered by our chief powder metallurgists and international procurement directors.
Explore additional precision sintered bronze bearings, MIM watch hardware, diesel aftermarket rebuild kits, and high-precision CNC finishing parts.






Send us your 2D PDF drawings and 3D STEP files today. Our engineering team will review your part geometry, recommend the optimal PM, MIM, or die-casting process route, and provide a full factory-direct quote within 48 hours.
Strict Confidentiality Assured: Non-Disclosure Agreements (NDAs) signed prior to file transfer. ISO 9001 & IATF 16949 Certified Operations.