
Engineered Tooling & Custom Molded Components
Explore our top-tier powder metallurgy compacting dies, MIM components, and die-casting solutions manufactured strictly to ISO 9001 and IATF 16949 quality benchmarks.







Global Landscape of Powder Metallurgy Molds & Tooling
The global powder metallurgy (PM) tooling industry forms the backbone of modern mass production for near-net-shape metal components. As automotive OEM manufacturers, aerospace system integrators, medical device developers, and industrial equipment builders strive for higher energy efficiency, reduced scrap rates, and localized strength customization, reliance on custom powder metallurgy compacting molds and Metal Injection Molding (MIM) tooling dies has reached an unprecedented scale.
A Powder Metallurgy Mold is far more than a simple cavity; it is a highly sophisticated, high-pressure mechanical unit subject to multi-directional compaction pressures ranging from 400 MPa to over 800 MPa. The mold assembly encompasses upper and lower punches, core rods, die plates, floating adapters, and ejection mechanisms engineered with micro-inch tolerances (often within ±0.002 mm to ±0.005 mm). These molds must withstand millions of high-tonnage compaction cycles while resisting severe abrasive wear, galling, micro-cracking, and mechanical fatigue caused by fine metallic powders under extreme friction.
Technical Information Gain: Advanced PM mold engineering now integrates sub-micron grain size Tungsten Carbide (WC-Co) cores, CPM 10V/15V particle metallurgy steel inserts, and dynamic finite element analysis (FEA) to eliminate micro-deflections during the green-part compaction phase, thereby extending tool life by up to 300% over conventional tool steel dies.
Utilizing high-cobalt tungsten carbide grades with grain sizes below 0.5 μm to guarantee maximum compressive strength and corrosion resistance against aggressive lubricant additives in metal powder blends.
Incorporating precise volumetric expansion and sintering shrinkage coefficients (typically 12% to 18% for MIM and 0.2% to 0.6% for press-and-sinter PM) directly into the CAD mold cavity geometry.
Designing complex split-punch systems and hydraulic floating die platforms to achieve consistent green density across stepped parts, gear teeth, and thin-wall structural features.
China Factory Efficiency & Structural Cost Advantages
Why leading tier-1 automotive suppliers and Fortune 500 equipment OEMs partner with Ningbo and Yangtze River Delta powder metallurgy mold manufacturers.
Global procurement directors face continuous pressure to balance rigid dimensional compliance with aggressive total cost of ownership (TCO) objectives. China’s powder metallurgy mold manufacturing ecosystem—particularly centered in high-tech industrial hubs like Ningbo, Zhejiang—offers unequaled operational agility, technological capabilities, and economic efficiency.
Within a 50-kilometer radius of our Ningbo facility, every critical sub-process—from specialized powder metallurgy steel stockholding, sub-micron carbide rod synthesis, specialized vacuum heat treating, to PVD nano-coating centers (TiAlN, DLC)—is fully integrated, eliminating lead-time bottlenecks.
Our machining workshops house Makino EDM machines, Sodick wire-cutting units, and Studer CNC cylindrical grinders. Operating 24/7 with automated robotic loading, we achieve lower machine-hour overheads while ensuring repeatable micron-level concentricity.
Through optimized tool steel allocation, modular mold base standardization (DME/HASCO compliant), and highly skilled toolmakers, we offer high-grade compaction tooling at a fraction of North American or Western European tooling costs.
Comparative Process Analysis: Powder Metallurgy Tooling vs. Alternative Manufacturing Molds
Understanding where powder metallurgy tooling fits relative to die casting molds, plastic injection molds, and subtractive CNC tooling is vital for selecting the optimal production path:
| Tooling Parameter | Powder Metallurgy (PM) Molds | Metal Injection Molding (MIM) Dies | Aluminum Die Casting Dies | Subtractive CNC Machining |
|---|---|---|---|---|
| Tooling Stress Level | Extreme High Pressure (400–800 MPa Compacting) | Moderate Pressure (50–150 MPa Injection) | High Impact & Thermal Shock (30–100 MPa) | Low (Cutting Tool Force Only) |
| Primary Tool Materials | Tungsten Carbide, CPM 10V, DC53, SKD11 | S136, H13, 1.2083 Stainless Die Steel | H13, 1.2344, Dievar Tool Steel | No Mold Required (Fixtures Only) |
| Part Material Suitability | Iron-Copper, Sintered Bronze, Alloy Steel | 316L, 17-4PH, Titanium, Low-Alloy Steels | A380, ADC12, Zamak Zinc Alloys | Virtually All Metals & Plastics |
| Part Geometric Complexity | Moderate to High (Axial stepped profiles, gears) | Extreme High (Undercuts, threads, micro-wall) | High (Housings, structural covers, thin ribs) | Limited by tool access/reach |
| Material Utilization Rate | 95% – 98% (Near-Zero Scrap) | 95% – 97% (Runner system recycled) | 85% – 90% (Gating trimmed & recast) | 15% – 50% (High scrap chips) |
| Typical Tooling Life | 500,000 – 2,000,000 strokes | 300,000 – 1,000,000 shots | 100,000 – 200,000 shots | N/A (Cutter replacement only) |
Localized Application Scenarios & Field Use Cases
From automotive powertrain gears to surgical jaw mechanisms, our custom powder metallurgy dies and MIM components perform under demanding operational conditions.
Scenario: Variable Valve Timing (VVT) rotors, oil pump gears, and planetary gearbox components require high density, low noise, and extreme wear tolerance.
Tooling Solution: Tungsten carbide die cavities engineered with spiral gear tooth EDM inserts and multi-stage split punches, delivering green part tooth alignment within DIN 7 accuracy standards.
Scenario: Laparoscopic surgical articulation joints, stapler jaws, and titanium implants require complex 3D shapes in 17-4PH stainless steel or Ti-6Al-4V.
Tooling Solution: Multi-cavity MIM molds featuring automatic side-core pullers, micro-ejection pins, and mirror-polished runners to prevent part distortion during automatic robotic pick-and-place.
Scenario: Ultra-thin hinge mechanisms, smartwatch cases, and camera bezel rings demanding cosmetic perfection, zero burrs, and tight tolerances (±0.01 mm).
Tooling Solution: Hot-runner MIM tooling constructed from ASSAB S136 stainless steel hardened to HRC 54–56, integrated with conformal cooling channels for minimum cycle time.
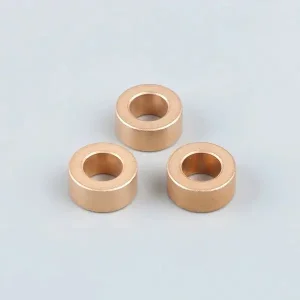
Scenario: Self-lubricating oil-impregnated bronze bearings, power tool gear heads, and hydraulic valve spools exposed to continuous friction.
Tooling Solution: Sintered powder metallurgy compacting dies with high-precision core rods manufactured to 0.001 mm roundness, giving optimal oil retention porosity.
Technological Trends Reshaping PM Mold Manufacturing
How modern tooling suppliers combine AI simulation, nano-coatings, and additive manufacturing to set new performance benchmarks.
The powder metallurgy mold manufacturing sector is undergoing a massive digital transformation driven by Industry 4.0 innovations. Legacy trial-and-error mold design methods have been superseded by predictive computational models and advanced material synthesis.
1. Finite Element Compaction Simulation (FEA & Moldflow)
Before cutting steel, our tooling engineers conduct rigorous powder compaction simulations (utilizing ANSYS and specialised PM simulation software). This models powder flow dynamics, friction distribution, and elastic tool deflection under 600+ MPa loads. Potential stress concentrations that cause premature die cracking or non-uniform green part density are identified and corrected at the CAD stage.
2. 3D Metal Printed Conformal Cooling for MIM Tooling
By leveraging Selective Laser Melting (SLM) metal 3D printing technology, we fabricate hardened tool inserts with internal conformal cooling channels that closely follow complex cavity contours. This reduces MIM molding injection cycle times by 20% to 35% while eliminating localized hot spots that cause thermal distortion and uneven volumetric shrinkage.
3. Next-Generation PVD Nano-Structured Coatings
Applying physical vapor deposition (PVD) titanium aluminum nitride (TiAlN), chromium nitride (CrN), or Diamond-Like Carbon (DLC) coatings to punch faces and die walls reduces friction coefficients down to < 0.1. This significantly reduces ejection force requirements, prevents galling during high-speed compacting, and extends mold re-polishing intervals by three-fold.
Global Procurement & OEM Engineering Guide
Follow our streamlined 5-step procurement workflow designed to transition your technical drawings into mass-produced components with zero friction.
Provide 3D CAD models (STEP, IGES, X_T) alongside 2D engineering drawings (PDF with GD&T specs). Our engineering team performs a thorough Design for Manufacturability (DFM) review within 24–48 hours, highlighting draft angles, radius optimizations, and wall thickness uniformity.
Receive a fully itemized commercial proposal detailing mold base costs, cavity insert steel grades, estimated tool life guarantee, sample delivery lead times, and unit piece pricing across multiple volume tiers (e.g., 5k, 20k, 100k+ units/year).
Upon CAD sign-off, mold fabrication begins using high-speed CNC centers, wire EDM, and mirror-surface EDM. Initial T1 green parts and sintered prototypes undergo full CMM dimensional verification prior to air-freighting sample lots to your testing laboratory.
We submit complete Production Part Approval Process (PPAP) documentation, including dimensional inspection reports, material chemical certificates, heat treatment hardness logs, and capability study reports (Cpk > 1.33) prior to full-scale mass production.
Powder Metallurgy Mold Technical Q&A
Direct answers from our senior tooling engineers to assist your technical evaluation and purchasing decisions.
Explore Additional Custom OEM Manufacturing Capabilities
Browse our complete series of sintered mechanical components, die-cast housings, custom MIM connectors, and specialized hardware assemblies.





Ready to Optimize Your Powder Metallurgy Tooling & Component Costs?
Partner with Ningbo Jiehuang Chiyang Electronic Tech Co., Ltd. for engineering expertise, 48-hour DFM reviews, and cost-efficient OEM production.