
Featured Precision Powdered Metal Components
Explore our high-volume wholesale catalog of engineered sintered alloys, metal injection molded components, and custom powder metallurgy auto/industrial parts.
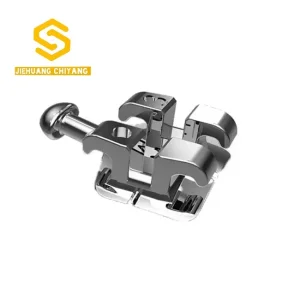
Wholesale dental supplies ortodoncia equipments MIM mesh base metal orthodontic MIM brackets Factory, Factories
View Product

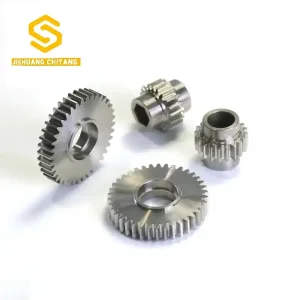
Wholesale 2019 Good Quality China Metal Injection Moulded Copper Base Gears for Automobile Parts Manufacturer, Suppliers
View Product
Wholesale Customized alloy metal metallurgy machinery sintered powder metallurgy auto parts Supplier, Factories
View Product
China Hot Sale for China Customized Powder Metallurgy Metal Injection Molding Parts Supplier, Factory
View Product
China Fast delivery MIM Mbt Bondable Self-Ligating Dental Orthodontic Bracket Manufacturers, Factories
View Product
Wholesale 2023 High quality Metal Injection Molding MIM Process for Titanium Alloy OEM Parts Factory, Factories
View ProductGlobal OEM Procurement Intent & Technical Sourcing Analysis
Modern supply chains demand a shift from subtractive machining to net-shape Powder Metallurgy (PM) and Metal Injection Molding (MIM) to optimize yield, reduce scrap, and achieve structural performance parity with wrought metals.
Key Buyer Sourcing Metrics & Pain Points
Global procurement directors, chief mechanical engineers, and automotive sourcing executives face unprecedented pressures to lower component unit costs without compromising tensile strength, fatigue resistance, or dimensional consistency. When sourcing precision powdered metal parts, technical evaluations typically focus on four core parameters:
- Metallurgical Density & Porosity Control: Achieving sintered densities upwards of 7.5 to 7.8 g/cm³ for structural iron-steel and stainless alloys, ensuring isotropic mechanical properties.
- Near-Net-Shape Geometric Complexity: Ability to produce complex 3D contours, internal threads, splines, and undercut features in a single compaction or sintering operation, eliminating multi-axis CNC secondary steps.
- Dimensional Repeatability: Maintaining Cp/Cpk values >1.67 across mass production runs exceeding 500,000 units per year.
- Total Landed Cost Optimization: Reducing raw material scrap rates from >60% (in sub-machining) down to <3% through closed-loop powder recovery systems.
Information Gain: High-Density PM vs. MIM Sourcing Choice
A frequent intent gap in wholesale component sourcing is misaligning the production technology with part mass and geometry. Our engineering roadmap clarifies the technological threshold:
- Powder Metallurgy (Press & Sinter): Optimal for 2.5D geometries, spur gears, timing pulleys, self-lubricating bushings, and high-torque structural parts up to 150mm in diameter or weights from 10g to 2.5kg. Uses mechanical or hydraulic presses (100 to 1,000 tons).
- Metal Injection Molding (MIM): Ideal for micro-to-small 3D complex components (<100g typical mass) with wall thicknesses as thin as 0.5mm, such as dental brackets, medical surgical tools, automotive VVT rotors, and smartphone hinges.
| Manufacturing Process | Typical Density (% Relative) | Dimensional Tolerance | Geometric Complexity | Raw Material Utilization | Economic Volume Threshold |
|---|---|---|---|---|---|
| Powder Metallurgy (Press & Sinter) | 85% - 95% (Up to 98% with Double Press/Sinter) | ±0.02mm to ±0.05mm | Medium (Axisymmetric, Gears, Stepped Profiles) | >95% | >5,000 pcs / order |
| Metal Injection Molding (MIM) | 96% - 99.5% (Wrought-Equivalent) | ±0.03mm to ±0.005mm (Post-sizing) | Ultra-High (Complex 3D, Under-cuts, Micro-holes) | >97% | >2,000 pcs / order |
| 5-Axis CNC Machining | 100% (Solid Bar Stock) | ±0.002mm to ±0.01mm | High (Constrained by Tool Reach) | 15% - 40% (High Scrap) | 1 to 1,000 pcs |
| Investment Casting (Lost Wax) | 92% - 96% (Porosity Risks) | ±0.10mm to ±0.20mm | High (Rougher Surface Finish) | 60% - 70% | >500 pcs |
Industry Trends & Technological Evolution in Precision Powdered Metals
The precision powdered metal industry is undergoing a systemic evolution fueled by electrification, medical device miniaturization, ultra-fine powder metallurgy, and green sintering technology.
1. Electrification & EV Powertrain Shift
The global shift toward Electric Vehicles (EVs) is altering powder metallurgy demand. While traditional Internal Combustion Engine (ICE) valve train parts are tapering, high-torque planetary gears, soft magnetic composites (SMCs) for traction motors, thermal management copper-base sintered heat sinks, and electronic power steering (EPS) sensors are growing exponentially. SMC materials permit 3D magnetic flux paths with ultra-low eddy current losses at high operational frequencies.
2. Titanium & Superalloy MIM (TiMIM)
Aerospace and medical technology sectors are accelerating the adoption of Titanium Metal Injection Molding (Ti-6Al-4V and Commercially Pure Titanium). Advanced gas-atomized spherical titanium powders coupled with ultra-clean vacuum debinding eliminate oxygen pick-up, achieving tensile strengths exceeding 900 MPa and bio-compatibility compliant with ASTM F2885 standards for surgical implants and lightweight drone actuators.
3. Micro-MIM & Ultra-Thin Walls
Demand for sub-gram components (<0.1g) with micro-features (such as micro-fluidic channels, self-ligating orthodontic bracket slots at 0.018-inch tolerances, and minimally invasive endoscopic jaws) has driven the deployment of ultra-fine metal powders (D50 < 5μm). These powders allow surface finishes of Ra 0.8μm directly out of the sintering furnace.
4. Digital Twin Sintering Simulation
To overcome anisotropic volumetric shrinkage during sintering (typically 12% to 20% linear shrinkage in MIM), leading powder metallurgy factories utilize finite element simulation software. By modeling gravity deformation, thermal gradient friction, and viscous sintering flow, mold dies are reverse-distorted during design, cutting tooling iteration cycles from 5 rounds down to 1.
5. Hybrid Additive-Sintering Manufacturing
Bridging rapid prototyping and high-volume wholesale production, modern factories deploy Binder Jetting (BJT) alongside traditional MIM. Using identical metal powders and vacuum sintering furnaces, engineers can prototype fully dense production-grade steel parts in days before cutting hard tool steel injection molds.
6. Sustainable Low-Carbon Metallurgy
Industrial buyers prioritize green suppliers. Energy-efficient continuous mesh belt sintering furnaces powered by hydrogen-nitrogen atmosphere gas generators reduce greenhouse gas emissions by up to 40% compared to legacy endothermic gas generators while providing cleaner carbon control in alloy steels.
Macro Industry Solutions & Process Engineering Framework
From raw elemental powder formulation to computer-controlled continuous sintering and secondary precision CNC machining, our holistic process guarantees structural integrity.
Phase 1: Powder Metallurgy (PM) Tooling & Compaction
For high-volume structural components like automotive timing sprockets, oil pump rotors, and shock absorber valves, mechanical compaction provides fast cycle times (10 to 30 strokes per minute).
- Material Formulations: Pre-alloyed iron powders, Fe-Cu-C mixes, diffusion-alloyed steels, nickel-steels (MPIF Standard 35 compliant).
- High-Pressure CNC Compaction: Multi-level 1,000-ton CNC hydraulic presses control powder filling across varying cross-sectional heights, preventing density gradients in green compacts.
- High-Temperature Sintering: Sintering at 1,120°C to 1,280°C under endothermic or dissociated ammonia atmospheres bonds powder particles via solid-state diffusion.
Phase 2: Metal Injection Molding (MIM) Lifecycle
For ultra-complex 3D shapes where conventional pressing is physically impossible due to side holes or undercuts, MIM combines plastics injection versatility with metal strength.
- Feedstock Preparation: Fine metal powders (316L, 17-4PH, 4140, Ti-6Al-4V) are compounded with thermoplastic and wax binder systems (typically 60% metal powder by volume).
- Precision Molding: Injection into multi-cavity hardened tool steel molds forms the "green part".
- Debinding & Vacuum Sintering: Catalytic nitric acid or solvent debinding removes the wax binder to create a "brown part". Subsequent vacuum sintering at up to 1,380°C shrinks the component to full theoretical density (>98%).
Comprehensive Secondary Operations & Surface Engineering
To meet extreme drawing requirements, wholesale powder metal component manufacturing is supplemented by internal finishing capabilities:
Quality Assurance, Quality Control (QA/QC) & Global Compliance
Reliability is paramount. Every batch of powder metal parts shipped to North America, Europe, or Asia-Pacific undergoes stringent metallurgical validation and digital CMM inspection.
IATF 16949 & ISO 9001 Systems
Our production facilities operate under full automotive Quality Management System (QMS) protocols. We provide comprehensive PPAP (Production Part Approval Process) Level 3 documentation, including Process Flow Diagrams, PFMEA, Control Plans, MSA studies, and full dimensional inspection records.
Advanced Metrology Lab
Equipped with Zeiss 3D Coordinate Measuring Machines (CMM), Keyence optical profilometers, metallographic micro-hardness testers (Vickers/Rockwell), Archimedes density testing balances, and X-ray fluorescence (XRF) alloy analyzers for total material traceability.
Environmental & IP Protection
Full compliance with RoHS 3, REACH, and Conflict Minerals regulations. Strict non-disclosure agreements (NDAs) and localized client service teams ensure customer CAD designs, proprietary alloys, and patented component profiles are protected.
Frequently Asked Questions (FAQ) for Engineering Buyers
Direct technical answers from our senior powder metallurgy engineers to help you evaluate design feasibility and procurement workflows.
What minimum wall thickness can be achieved with Metal Injection Molding (MIM)?
MIM components can reliably achieve nominal wall thicknesses as thin as 0.5mm (0.020 inches), and micro-MIM processes can produce localized ribbing down to 0.3mm. However, uniform wall thickness is recommended across the part geometry to prevent differential cooling during binder removal and distortion during vacuum sintering.
How do mechanical properties of MIM parts compare to machined bar stock?
Sintered MIM parts routinely reach 96% to 99.5% relative density compared to theoretical wrought density. Consequently, key mechanical properties—such as yield strength, ultimate tensile strength, and hardness—are virtually identical to machined wrought metals (e.g., 17-4PH H900 reaching tensile strengths >1,150 MPa). For ultra-critical structural loads, Hot Isostatic Pressing (HIP) can eliminate 100% of residual micro-porosity.
What are the standard production lead times for tooling and initial samples?
For conventional powder metallurgy press tooling, design and mold build require approximately 25 to 30 days. For complex multi-cavity MIM tooling, tool construction and first-article inspection (FAI) sample submission take 30 to 40 days. Rapid metal 3D printing or binder jetting prototypes can be provided in 5 to 7 days for preliminary design verification.
What is the typical Minimum Order Quantity (MOQ) for custom components?
Due to the tooling setup costs and high-temperature furnace economics, standard MOQs are 2,000 pieces for MIM and CNC finished parts, and 5,000 pieces for standard press-and-sinter powder metallurgy components. However, for specialized titanium (TiMIM) or high-value medical components, smaller pilot production runs can be accommodated.
Which metal alloys are available for custom wholesale manufacturing?
Our material portfolio includes Stainless Steels (316L, 17-4PH, 304L, 420, 440C), Low-Alloy Carbon Steels (4140, 4340, 8620, Fe-Ni alloys), Titanium Alloys (Ti-6Al-4V, CP-Ti), Soft Magnetic Alloys (Fe-Si, Fe-Ni, Fe-Co), Copper/Brass Alloys, Tool Steels (M2, SKD11), and High-Temperature Ceramics (Zirconia, Alumina).
How does the unit cost of powder metallurgy compare to die casting?
Die casting is ideal for non-ferrous metals like aluminum and zinc when low density and structural housing geometry are needed. However, die casting cannot cast high-strength steel, stainless steel, or titanium alloys due to melting point constraints. Powder metallurgy and MIM provide high-strength ferrous components with zero material contamination and far greater wear resistance.
Advanced Custom Sintered Components & Machinery Hardware
Browse our specialized factory line of sintered sleeves, industrial motor hardware, ceramic wire connectors, and high-precision machinery spare parts.

Wholesale Reasonable price Powder Metallurgy Company Custom Powder Metallurgy Products Manufacturers, Supplier
View Product

China Price Sheet for China Powder Metallurgy Motor Shaft Sleeve Metal Powder Sintered Parts Supplier, Factories
View Product
China Manufacturer Custom Metal Brass Zinc Die Casting Mould Parts Anodizing Aluminum Die Casting Suppliers, Factory
View Product
Wholesale PriceList for Custom Sintering Metal Injection Molding MIM Hardware for CNC Machinery Auto Parts Manufacturer, Factories
View Product
China Ordinary Discount Custom Metal Injection Molding Stainless Steel Parts for Complex CNC Metal Components Sintering Metal Parts for Machinery Spare Parts Manufacturers, Factories
View Product
Request an Engineering DFM & Wholesale Quotation
Send us your 2D (PDF) and 3D (STEP/IGES) CAD models. Our senior powder metallurgy engineering team will perform a free Design for Manufacturability (DFM) review and deliver a complete tooling & component cost quote within 48 hours.