
Core Sintered Components & Precision Hardware
Direct factory supply of precision powder metallurgy, timing gear rings, MIM structural components, and die-cast solutions.

China Factory Directly supply Sintered Steel Timing Gear Rings Custom Die Casting Parts Manufacturers, Factory

China One of Hottest for Factory OEM Metal Die Casting Part Aluminum Die Casting CNC Machining Large Flywheel Housing Aluminum Replaces Manufacturers, Supplier

China Ceramic seal Supplier, Factories

China Discount wholesale China Powder Metallurgy Customized Components Sintered Spare Parts Manufacturers, Suppliers
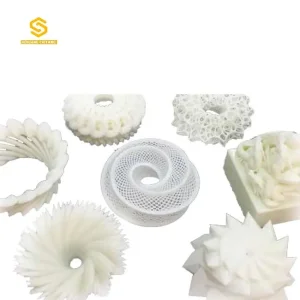
China 3D Printing Manufacturer, Manufacturers
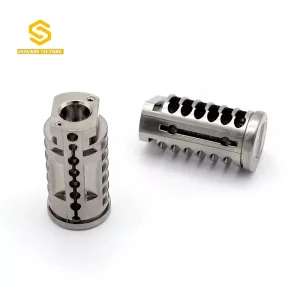
Wholesale Metal Injection Molding Locking Technology Factory, Factories

Wholesale china aluminium pressure die casting housing manufacturer Manufacturer, Supplier

Wholesale High Quality MIM Metal Injection Molding Process High Volume Production for Metal Parts for Customized CNC Precision Turning Milling Stainless Steel Parts Machinery Parts Manufacturer, Manufacturers
The Engineering & Metallurgical Foundations of Sintered Gears
Delivering Information Gain through density optimization, pore structure control, and near-net-shape powder metallurgy metallurgy.
Density & Pore Morphometry
Sintered gear performance correlates directly with localized density. Standard press-and-sinter achieves densities between 6.8 g/cm³ and 7.2 g/cm³, whereas advanced warm compaction and surface rolling push tooth-root densities beyond 7.55 g/cm³. By controlling pore morphometry—rounding sharp interparticle voids—fatigue resistance increases up to 35% under cyclic bending loads.
Alloy Systems & Microstructures
Utilizing pre-alloyed and diffusion-alloyed steel powders (MPIF 35 specifications such as FL-4405, FD-0205, and FN-0208), sintered gears undergo controlled phase transformations during sintering. Liquid-phase sintering coupled with rapid sintering-hardening yields a predominantly martensitic matrix with fine carbondiffused pearlite, ideal for high-impact power transmission.
Near-Net-Shape Geometric Efficiency
Compared to traditional gear hobbing or shaping where up to 40% of bar stock is turned into scrap chips, powder metallurgy (PM) and Metal Injection Molding (MIM) achieve material utilization rates exceeding 95%. Complex features such as internal splines, dual-gear clusters, and helical angles up to 25° are formed in a single pressing stroke.
Metallurgical Insight: Grain Boundary Engineering in Sintering
In high-torque industrial transmissions, gear tooth failure predominantly initiates at sub-surface stress concentrations caused by irregular residual porosity. As a premier wholesale sintered gears supplier, our manufacturing facilities deploy high-temperature mesh belt furnaces operating up to 1280°C under dissociated ammonia or synthetic endothermic atmospheres (N₂/H₂ blend). This precise thermodynamic control eliminates surface decarburization, promotes complete neck formation between iron particles, and guarantees DIN 3962 Class 8 to Class 10 gear accuracy natively, upgradable to Class 6 through post-sinter surface rolling.
Localized Application Scenarios for Sintered Gears
From automotive powertrain sub-assemblies to smart robotics, discover how engineered powder metal gears operate in mission-critical environments.
Automotive Powertrains & VVT Systems
Sintered steel timing gear rings, Variable Valve Timing (VVT) sprockets, and variable displacement oil pump rotors operate continuously under elevated thermal shocks (150°C) and cyclic engine vibration. High-density sintered iron-nickel alloys ensure silent mesh performance, reduced inertia, and zero-defect fatigue lifespans across 200,000+ kilometers.
Heavy Industrial & Power Tool Gearboxes
Cordless power tools, lawn tractors, and industrial actuators demand massive power density in ultra-compact envelopes. Sintered planetary gear systems featuring dual-stage reduction gears handle dynamic stalling torque up to 120 Nm. Vacuum oil-impregnation options eliminate periodic maintenance while serving as internal self-lubricating reservoirs.
Robotics & Medical Actuation Systems
For surgical automation, exoskeletons, and collaborative robot joint reducers, micro-MIM gears made from 17-4PH or 316L stainless steel offer tooth module sizes as small as m0.15. These precision-sintered components yield backlash angles under 3 arc-min without requiring multi-axis secondary CNC gear grinding.
Sintered Gear Technology Roadmap (2025–2030)
How advanced materials science and digital manufacturing are redefining powder metallurgy transmission efficiency.
Roll Densification & Hobbing Integration
Implementation of dual-roll CNC densification equipment to transform root and flank pore fractions down to <1%, exceeding wrought alloy strength limits for heavy EV gearboxes.
Binder Jetting + PM Sintering
Integration of industrial metal binder jetting (BJAM) with conventional vacuum sintering to eliminate tooling lead times for low-volume custom gear prototyping.
AI-Driven Optical & Acoustic Inspection
Deployment of 100% in-line visual and resonant frequency testing (NDT) powered by AI vision algorithms to instantly isolate internal micro-cracks or density variations.
Next-Gen Alloy Powders
Adoption of nano-structured alloy powders reducing sintering temperatures by 150°C while achieving 99.2% theoretical density without secondary pressing.
China Supply Chain Resilience & Cost-Efficiency Architecture
Leveraging Ningbo's world-class manufacturing ecosystems, automated press technology, and rapid DFM execution.
Integrated Industrial Cluster Synergy
Located in the heart of Zhejiang’s advanced hardware hub, our production infrastructure benefits from immediate proximity to elemental metal powder atomization plants, tool steel die specialists, and heat-treatment facilities. This localized cluster shrinks material lead times by 60% compared to fragmented Western supply lines.
Automated Multi-Cavity Press Capacity
Operating high-tonnage automated mechanical and hydraulic presses (up to 1,000 Tons / 10,000 kN capacity) equipped with multi-level CNC die sets. We routinely mold complex stepped gears and multi-track timing sprockets in 4-cavity tooling, achieving production outputs of over 100,000 units per shift.
48-Hour DFM & Fast Tooling Turnaround
Our senior metallurgical engineering team delivers thorough Design for Manufacturability (DFM) reviews within 48 hours. By utilizing wire-EDM, high-speed CNC mold milling, and internal CMM validation, customized prototype tooling is ready for sampling within 18–25 days.
Process Comparison: Sintered vs MIM vs Die Casting vs Hobbing
Objective technical analysis to assist engineering buyers in selecting the optimal process path for custom transmission parts.
| Evaluation Parameter | Powder Metallurgy (PM) | Metal Injection Molding (MIM) | Aluminum/Zinc Die Casting | Traditional CNC Hobbing |
|---|---|---|---|---|
| Primary Target Geometry | Spur gears, sprockets, 2.5D profile steps | Small, ultra-complex 3D gears, micro-teeth | Lightweight housings, thin-wall frames | Rotational shafts, external gear profiles |
| Typical Density Range | 6.8 – 7.4 g/cm³ (up to 7.6 with rolling) | 7.5 – 7.8 g/cm³ (96-99% solid) | 2.7 – 6.6 g/cm³ (Alloy dependent) | 7.85 g/cm³ (Fully solid wrought stock) |
| Dimensional Accuracy | DIN 3962 Class 8–10 (IT 7-9) | DIN 3962 Class 9–11 (IT 8-10) | IT 10–12 | DIN 3962 Class 6–8 (IT 5-7) |
| Material Yield Efficiency | 95% – 98% | 95% – 98% (Feedstock recyclable) | 90% – 95% (Sprues remelted) | 40% – 60% (High chip waste) |
| Economic Order Quantity (MOQ) | 5,000+ units | 2,000+ units | 2,000+ units | 1 – 500 units (Low tooling cost) |
| Unit Cost @ High Volume | Lowest | Low - Medium | Low | High (Tool wear & cycle time) |
Global Compliance & Localized Support Framework
Eliminating international procurement risk with rigorous quality management and clear commercial protection.
IATF 16949 & ISO 9001 Certifications
Our quality systems execute full APQP, PPAP Level III documentation, FMEA analysis, and SPC tracking. Every gear order includes raw material spectrometry certificates, heat-treatment microhardness charts, and 100% optical dimension scanning reports.
NDA Protection & IP Safeguarding
We routinely sign legally binding Non-Disclosure Agreements (NDAs) prior to examining technical drawings. CAD files stay encrypted on secure internal servers with restricted departmental access control protocols.
Door-to-Door Logistics & Local Warehousing
Complete export handling including DDP (Delivered Duty Paid) shipping options across North America, Europe, Japan, and Southeast Asia. We support consignment stocking and safety-stock buffers at regional hub facilities.
Additional Powder Metallurgy & Custom Cast Hardware
Explore our custom OEM manufacturing capabilities in zinc/aluminum die casting, titanium MIM, ceramic components, and precision CNC turning.

China OEM Metal Die Casting Products Custom Zinc Aluminum Alloy Die Casting Parts Manufacturer, Factories

Wholesale Customized alloy metal metallurgy machinery sintered powder metallurgy auto parts Supplier, Factories

China OEM Supply Sintered Powder Metallurgy Custom Metal Injection Molding Parts for CNC Machining Stainless Steel Components,Iron Plated Spare Parts for Machine Electric Device Manufacturer, Factory

Wholesale Ultra Titanium Case Parts Stainless Steel Watch Band Charms Manufacturers, Factory

China Discountable price Metal Injection Molding MIM Sintered Parts Manufacturer for Precision Machinery Steel Components Manufacturers, Factories

Wholesale Good Wholesale Vendors Factory Custom MIM Metal Injection Molding MIM Gear Part for Electronic Components Manufacturer, Manufacturers

China Ceramic Terminal Strip Manufacturer, Supplier
Wholesale Zirconia Ceramic Tube Manufacturer, Factories
Frequently Asked Questions by Technical Buyers
In-depth answers addressing engineering tolerances, minimum order quantities, surface treatments, and lead times.