
High-Precision Sintered & MIM Metal Components
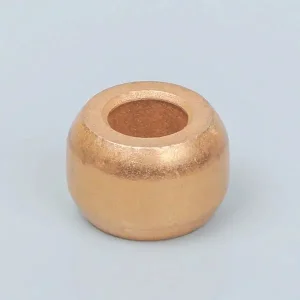
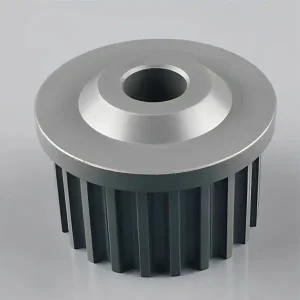
Explore our OEM powder metallurgy gear formulations, sintered bushings, and custom metal injection molding (MIM) structural parts.




Redefining Torque Transmission: The Engineering Science Behind Sintered Metal Gears
In modern high-duty mechanical systems, the transition from traditional subtractive CNC gear machining to high-density Powder Metallurgy (PM) and Metal Injection Molding (MIM) gear manufacturing represents a fundamental shift in total procurement efficiency. As a tier-one Wholesale Sintered Metal Gears Manufacturer & Supplier, Ningbo Jiehuang (JHMIM) bridges advanced material science with precision mechanical engineering to deliver net-shape and near-net-shape gear solutions.
Sintered metal gears are produced by compacting elemental or alloyed metal powders inside high-precision carbide dies under extreme pressure (400–800 MPa), followed by high-temperature solid-state sintering under controlled synthetic atmospheres ($1120^\circ\text{C} - 1280^\circ\text{C}$). The resulting microstructure yields exceptional dimensional repeatability, inherent self-lubricating porosity, and mechanical properties tailored for arduous duty cycles.
Core PM Gear Engineering Advantages
- Material Utilization: Exceeds 95% (vs. 40-50% in CNC turning/hobbing).
- Geometric Complexity: Direct molding of dual gears, internal splines, and eccentric cams.
- Acoustic Damping: Controlled micro-porosity reduces tooth contact noise (NVH) by 3-5 dB.
- Cost Reduction: 30% to 55% landed cost savings on high-volume production.
Technical Manufacturing Benchmarks
Quantifiable engineering performance delivered across our sintered gear production lines
1. Global Procurement Demands for Sintered Metal Gears
Analyzing Total Cost of Ownership (TCO), material efficiency, and localized risk mitigation in global OEM component sourcing.
Global TCO Optimization
Global original equipment manufacturers (OEMs) in North America, Europe, and Asia-Pacific face relentless pressure to reduce unit costs without sacrificing gear durability. Sintered metal gear manufacturing eliminates costly multi-axis machining operations, gear shaping, hobbing, and deburring. By delivering fully net-shape gear geometries straight from the furnace, buyers achieve dramatic reductions in Total Cost of Ownership (TCO).
High Material Conservation & Sustainability
With global ESG standards mandating carbon footprint mitigation across tier-1 supply chains, powder metallurgy serves as a benchmark green technology. Traditional gear cutting turns up to 50% of alloy steel stock into scrap metal swarf. Sintering achieves over 95% material utilization, lowering raw material consumption and minimizing energy footprint per gear produced.
Supply Chain Resilience & Rapid Scalability
Wholesale procurement requires stable manufacturing capacity capable of absorbing demand spikes. Modern PM gear production utilizes multi-cavity tooling running on automated high-tonnage hydraulic presses. Able to output thousands of high-precision gear components per hour, sintered metallurgy protects global product launches against capacity bottlenecks.
2. Macro Industry Solutions & Tailored OEM Applications
Deploying customized powder metal gear formulations across critical global industrial sectors.
Automotive Powertrain & EV Systems
In internal combustion engine (ICE) and Electric Vehicle (EV) platforms, sintered metal gears are vital for Electronic Power Steering (EPS), Variable Valve Timing (VVT) phasers, oil pump rotors, brake vacuum actuators, and seat adjustment mechanism gearboxes. High-density sinter-hardened alloys withstand cyclic impact loads while offering superior acoustic absorption.
Robotics & Precision Motion Control
Smart factory automation, AGV wheel drives, and joint actuators demand miniature planetary gearboxes with high torsional stiffness and zero backlash. Utilizing micro-powder metallurgy and Metal Injection Molding (MIM), we fabricate spur gears, sun gears, and internal ring gears down to Module 0.2 with high AGMA accuracy.
Heavy-Duty Cordless Power Tools
High-torque cordless drills, impact wrenches, and rotary hammers rely heavily on multi-stage planetary gear systems. Sintered nickel-steel and copper-steel gears provide exceptional tooth shear strength, resisting extreme peak shock forces when power tools stall or reverse instantly under high load.
Medical Devices & Surgical Instruments
Modern surgical robotics, peristaltic dosing pumps, and automated diagnostic gear trains require micro-scale stainless steel gears (316L, 17-4PH) that resist aggressive sterilization fluids. MIM sintering allows bio-compatible alloy gears to be produced with intricate structural features in single-step operations.
Hydraulic & Lubrication Pump Rotors
Gerotor oil pumps and internal hydraulic gear drives require high volumetric efficiency. Precision press-and-sinter technology creates smooth trochoidal tooth profiles that maintain tight tip sealing tolerances, minimizing fluid bypass and cavitation in heavy machinery hydraulic systems.
Smart Home Appliances & HVAC Controls
From silent automated window actuators to kitchen food processor gear transmissions, oil-impregnated sintered bronze and iron gear assemblies provide maintenance-free lifetime self-lubrication with whisper-quiet operating acoustics.
3. Technical Roadmap: Powder Metallurgy & Sintering Science
An engineering breakdown of powder alloy formulation, compaction physics, surface densification, and sinterhardening.
Advanced Powder Preparation & Alloy Selection
The mechanical performance of a sintered gear begins at the atomic level. We utilize diffusion-alloyed and pre-alloyed steel powders (containing Ni, Mo, Cu, Cr, and C) to guarantee microstructural homogeneity. Powder compressibility is optimized through organic lubricant binders, enabling uniform compaction density across complex gear teeth.
Multi-Axial CNC Powder Compaction
Utilizing high-tonnage automated presses (up to 1,000 tons / 10,000 kN), powder is pressed into carbide dies. Multi-level tool adapters independently control the movement of upper and lower punches, eliminating density gradients between the gear hub, web, and gear teeth to prevent distortion during sintering.
Atmosphere-Controlled Sintering & Sinterhardening
Green gears pass through multi-zone continuous mesh-belt furnaces under a protective endothermic or nitrogen-hydrogen atmosphere ($90\% \text{ N}_2 / 10\% \text{ H}_2$). In-furnace sinterhardening rapidly cools the gears directly from sintering temperature ($>850^\circ\text{C}$) at rates exceeding $2-5^\circ\text{C/s}$, transforming the matrix into fine martensite without secondary quench oil distortion.
Surface Densification & Tooth Rolling
To rival the contact fatigue strength of wrought steel, critical gears undergo secondary surface rolling densification. Precision rolling dies cold-work the gear tooth roots and flanks, closing surface pores to achieve near 100% theoretical density ($7.8 \text{ g/cm}^3$) in the load-bearing stress zone up to a depth of 1.0 mm.
Comparative Engineering Data: Popular PM Gear Materials (MPIF Standard 35)
| Material Designation | Composition Alloy Type | Sintered Density (g/cm³) | Tensile Strength (MPa) | Yield Strength (MPa) | Apparent Hardness | Typical OEM Gear Application |
|---|---|---|---|---|---|---|
| MPIF FN-0208 | Iron-Nickel Steel (2% Ni, 0.8% C) | 6.8 - 7.2 | 450 - 650 | 350 - 480 | 75 - 88 HRB | General Industrial Spur & Bevel Gears |
| MPIF FLN2-4405 | Hybrid Prealloyed Steel (Ni-Mo-C) | 7.1 - 7.4 | 780 - 1100 | 650 - 850 | 32 - 42 HRC | High-Torque Automotive Steering & Timing Gears |
| MPIF FC-0208-50 | Copper-Steel (2% Cu, 0.8% C) | 6.6 - 7.0 | 400 - 550 | 320 - 420 | 65 - 80 HRB | Lawn & Garden Gearboxes, Appliance Components |
| MPIF FX-2008 | Copper-Infiltrated Iron-Steel | 7.2 - 7.5 | 600 - 850 | 450 - 600 | 80 - 95 HRB | Heavy Impact Power Tool Planetary Gears |
| MIM 17-4PH | Precipitation Hardening Stainless | 7.6 - 7.75 | 1150 - 1350 | 1000 - 1200 | 38 - 44 HRC | Corrosion-Resistant Medical & Aerospace Actuators |
*Data compiled under MPIF 35 standard test conditions. Custom heat treatment and resin impregnation available upon engineering review.
4. Global Business Landscape & Manufacturing Benchmark
Comparing Sintered Metal Gears against alternative gear manufacturing methodologies.
Sintered Metal Gears (PM / MIM)
- Cost at Volume: Extremely Low (Net-shape production).
- Production Speed: Up to 1,200 parts/hour per press.
- Feature Freedom: High (Splines, dual gears, keyways molded directly).
- Acoustics: Excellent micro-porous vibration absorption.
- Material Waste: Less than 5%.
Cut Machined Steel Gears (CNC / Hobbed)
- Cost at Volume: High (Machining cycle time per unit).
- Production Speed: Slow (Multiple setups required).
- Feature Freedom: Limited by tool geometry access.
- Acoustics: Solid metal transmits high-frequency gear whine.
- Material Waste: 40% - 60% turning scrap.
Injection Molded Plastic Gears
- Cost at Volume: Low.
- Torque Capacity: Very Low (Prone to tooth shear & creep).
- Thermal Limit: Fails above 100°C - 120°C.
- Environmental Life: Degrades in presence of solvents & oils.
- Precision: High thermal expansion affects mesh backlash.
5. Quality Infrastructure, Certification & Localization Support
Ensuring zero-defect manufacturing compliance for international tier-1 OEM clients.
Certified Quality System
Our 28,000 m² Ningbo manufacturing plant operates strictly under IATF 16949:2016 automotive quality standards and ISO 9001:2015. Every production batch undergoes PPAP Level III documentation, FMEA analysis, and full lot-level traceability.
Advanced Inspection Lab
Equipped with Zeiss 3D Coordinate Measuring Machines (CMM), Osaka Gear Measuring Instruments (GMC), Scanning Electron Microscopes (SEM), density testing pycnometers, and automated optical sorters to guarantee 100% key dimensional compliance.
Global DFM & Logistics Support
Our multi-lingual engineering office provides rapid Design for Manufacturability (DFM) reviews within 48 hours. We handle EXW, FOB, CIF, DDP shipping terms to North America, EU, Japan, and Southeast Asia with seamless customs clearing support.
Additional Sintered Assemblies & Die Casting Hardware
Discover specialized engine rotors, MIM watch accessories, and high-pressure die casting tooling solutions.





6. Frequently Asked Questions (FAQ) & Technical Guidance
Direct engineering answers to technical procurement questions regarding sintered gear design, tolerances, and mechanical capabilities.
Partner with a World-Class Sintered Metal Gear Manufacturer
Send us your 2D (PDF) and 3D (STEP/IGES) CAD models today. Our engineering team will return a comprehensive Design for Manufacturability (DFM) analysis and a transparent quotation within 48 hours.