
Sintered Ceramic Components & Powder Metallurgy Assemblies
Explore our certified catalog of high-density sintered parts, custom ceramic components, micro gears, and precision MIM structures built for extreme industrial operating environments.






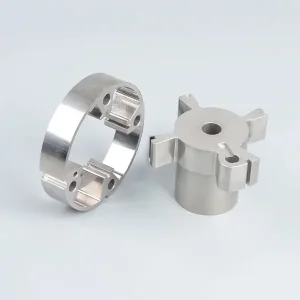

Sintering Ceramics Technology Roadmap & Thermal Processing Advances
Understanding solid-state diffusion, liquid-phase densification, and pressure-assisted consolidation protocols for next-generation structural and functional technical ceramics.
Spark Plasma Sintering (SPS / FAST)
Field-Assisted Sintering Technology utilizes pulsed direct electric current combined with uniaxial mechanical pressure to achieve rapid densification at temperatures up to 2,200°C. This technique limits grain growth, yielding nanostructured ceramic bodies with superior hardness and fracture toughness.
- Heating rates up to 1000°C/min
- Dwell times under 15 minutes
- Near 100% theoretical density ($>99.8\%$)
Hot Isostatic Pressing (HIP)
Post-sintering HIP applies inert argon gas pressure up to 200 MPa at elevated temperatures. By eliminating residual micro-porosity and grain boundary defects, HIP processing restores maximum mechanical integrity, making ceramics resilient against dynamic fatigue and thermal fatigue shocks.
- Elimination of internal closed pores
- Bending strength boost up to 40%
- Ideal for aerospace and bio-implants
Microstructural Grain Engineering
By controlling sintering atmosphere composition (high-purity hydrogen, nitrogen, or vacuum) and introducing nano-dopants (such as $MgO$ in Alumina or $Y_2O_3$ in Zirconia), microstructures are engineered to exhibit elongated grain interlocking, preventing catastrophic crack propagation.
- Sub-micron grain size distribution
- Enhanced transformation toughening
- Tailored dielectric breakdown voltage
Sintered Technical Ceramics Material Specifications
Compare mechanical, thermal, and electrical metrics across our core ceramic formulations to optimize component life cycle and operating reliability.
| Ceramic Material System | Density ($g/cm^3$) | Flexural Strength ($MPa$) | Vickers Hardness ($HV$) | Thermal Conductivity ($W/m\cdot K$) | Max Operating Temp (°C) | Primary Industrial Use Case |
|---|---|---|---|---|---|---|
| Alumina ($Al_2O_3$ 99.5%) | 3.92 | 380 - 450 | 1,600 | 30 | 1,650 | Electrical Insulators / Chemical Seals |
| Y-TZP Zirconia ($ZrO_2$) | 6.05 | 1,000 - 1,200 | 1,300 | 2.5 | 1,000 | Structural Shafts / Surgical Blades |
| Silicon Nitride ($Si_3N_4$) | 3.25 | 850 - 950 | 1,500 | 35 - 80 | 1,400 | EV Bearings / Turbocharger Rotors |
| Sintered Silicon Carbide ($SSiC$) | 3.15 | 420 - 500 | 2,400 | 120 - 180 | 1,600 | Semiconductor Chucks / Armor Tiles |
| Zirconia Toughened Alumina ($ZTA$) | 4.35 | 600 - 750 | 1,750 | 24 | 1,500 | High-Wear Valve Plates / Wear Rings |
Macro-Industry Solutions & Engineered Component Deployment
Custom OEM ceramic solutions engineered to replace failure-prone metal alloys under severe tribological, chemical, and thermal pressure.
Semiconductor & Wafer Processing Equipment
Wafer fabrication equipment requires ultra-high purity materials featuring zero outgassing, high dielectric strength, and extreme plasma erosion resistance. Our sintered SiC electrostatic chucks (ESC) and high-purity alumina chamber rings maintain micro-level flatness under fluorine and chlorine plasma environments.
- Sub-micron particle generation mitigation
- Dielectric breakdown strength up to 18 kV/mm
- Custom vacuum metallization and co-firing options
Automotive & Electric Vehicle (EV) Powertrains
High-voltage EV architectures demand superior electrical isolation combined with high thermal dissipation. Sintered Silicon Nitride ($Si_3N_4$) ceramic bearing balls prevent electrical pitting caused by stray shaft currents in 800V drive motors, extending bearing service life by up to 500% over steel alternatives.
- Lower rotational inertia compared to chrome steel
- Thermal barrier substrates for SiC power modules
- High thermal shock stability ($\Delta T = 800^\circ\text{C}$)
Aerospace Propulsion & Hypersonic Systems
Engineered Ceramic Matrix Composites (CMCs) and sintered Alumina-Silicate radomes maintain structural stiffness under aerodynamic heating up to 1,600°C. Low loss tangent dielectric properties ensure signal transparency for radar and guidance sensor windows.
- Lightweight structural design ($50\%\text{ mass reduction vs superalloys}$)
- High thermal oxidation resistance
- Low dielectric constant ($\varepsilon_r = 9.1 - 9.8$)
Chemical Fluid Handling & Extreme Wear Hardware
In harsh chemical processing, abrasive slurry pumping, and desorber valve mechanisms, traditional alloy valves erode rapidly. Our sintered Zirconia ($ZrO_2$) and Alumina ($Al_2O_3$) seal rings and plunger pistons provide complete immunity to acids and alkalis while exhibiting low friction coefficients.
- Zero chemical reactivity with concentrated $HCl$ and $H_2SO_4$
- Polished surface finish down to $Ra\ 0.05\ \mu m$
- Elimination of galling and micro-welding failures
China Smart Factory 4.0: Supply Chain Resilience & Cost Leadership
Combining automated powder synthesis, multi-cavity dry pressing, continuous vacuum sintering, and 100% automated optical inspection (AOI) to deliver unmatched price-performance ratios.
Closed-Loop IIoT Automation
Our Ningbo production facility leverages real-time temperature, pressure, and atmosphere telemetry monitored via edge computing sensors. This guarantees batch-to-batch thermal uniformity and eliminates thermal gradient warping in complex geometric profiles.
In-House Tooling & Rapid DFM
Integrated CAD/CAM mold development allows design-for-manufacturability (DFM) verification within 24 hours. Custom multi-cavity press tooling is produced in-house using high-speed CNC and wire-EDM equipment, shortening lead times from weeks to days.
Optimized Total Cost of Ownership (TCO)
By coupling localized raw ceramic powder synthesis with high-throughput continuous sintering kilns, we reduce per-unit energy and processing overhead, passing a direct 30% to 45% cost savings to global OEM buyers without sacrificing quality.
Global Supply Chain Compliance & Quality Assurance
Ensuring multi-tier quality inspection, strict IP protection, and full compliance with international standards for seamlessly integrated cross-border procurement.
Quality Certification & Traceability Standards
Our quality control laboratory is equipped with Zeiss Coordinate Measuring Machines (CMM), Keyence laser profile analyzers, and X-ray fluorescence (XRF) spectrometers. Every batch includes a comprehensive Certificate of Analysis (CoA).
- IATF 16949 automotive quality management compliance
- ISO 9001 certified manufacturing workflow
- Full material lot traceability with 10-year record retention
- RoHS 3.0, REACH, and Conflict Minerals certified
Localized Logistics, Buffer Stocking & IP Protection
We mitigate international supply disruption by supporting flexible commercial terms (FOB, CIF, DDP, DAP) combined with Vendor-Managed Inventory (VMI) buffer stocks hosted in North American and European logistics hubs.
- Strict Non-Disclosure Agreements (NDA) prior to CAD transfer
- Dedicated secure CAD data storage with air-gapped backups
- Safety stock maintenance for blanket OEM purchase orders
- Customized protective packaging (vacuum sealing & ESD protection)
High-Precision Sintered Parts & Die Casting Assemblies
Explore additional high-demand OEM products manufactured via powder metallurgy, metal injection molding (MIM), precision aluminum die casting, and specialized ceramic sealing technologies.


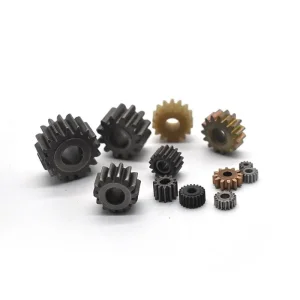




Sintering Ceramics Procurement & Engineering FAQ
Expert engineering responses to common queries regarding sintering ceramics tolerances, DFM guidelines, tooling lead times, and post-sintering finishing operations.
Request a Custom Ceramic Technical Quote & DFM Review
Send us your 2D engineering drawings (PDF) and 3D CAD models (STEP/IGES). Our senior engineering team will provide a DFM manufacturability analysis and transparent quotation within 48 hours.
Contact Our Technical Engineering Team