
Micro-Precision MIM Solutions for Italian Tech Brands
Engineered for extreme dimensional tolerances, intricate geometry, and premium aesthetic metal finishing.

Wholesale SIM Slot by Metal Injection Molding Manufacturer (Milan Mobile Tech Grade)
Ultra-thin wall (0.25mm) stainless steel SIM slots engineered with high mechanical strength and precise ejector pin tolerances for premium smartphones and IoT devices.
View Product Details
Custom MIM Stainless Steel Watch Buckles & Clasps Supplier (Milan Fashion-Tech Series)
Complex ergonomic watch buckles and deployment clasps crafted via 316L/17-4PH MIM. Ideal for luxury wearable tech and Milan fashion smartwatch integration.
View Product Details
China MIM For Stainless Steel Watch Frame Manufacturers (Milan Smart Wearable Spec)
High-density near-net-shape smartwatch bezels and structural internal frames offering mirror-polishing readiness, PVD coating compatibility, and IP68 sealing precision.
View Product Details
Wholesale Metal Injection Metallic CPU Cooling Fans & Micro Thermal Components
Intricate metallic fan impellers and mini thermal dissipators engineered for compact laptop servers, high-performance computing, and automotive electronics in Lombardy.
View Product DetailsTransforming Electronics Hardware Sourcing for Milan’s Industrial Leaders
The convergence of luxury aesthetics, industrial engineering, and next-generation smart electronics has positioned Milan and the broader Lombardy region as a premier European epicenter for consumer tech innovation. From high-end wearable biometric devices and luxury smart accessories to compact IoT modules and audiophile hardware, Italian design houses and original equipment manufacturers (OEMs) demand metal components that combine intricate geometric complexity with pristine cosmetic finishing.
This technical whitepaper examines how China’s Metal Injection Molding (MIM) manufacturing ecosystems—led by advanced ISO 9001 and IATF 16949 certified facilities like Ningbo Jiehuang Chiyang Electronic Tech Co., Ltd. (JHMIM)—deliver a decisive competitive advantage to Milanese product designers, hardware engineers, and procurement directors. By fusing plastic injection molding design freedom with wrought-metal material strength, Chinese MIM factories empower European brands to achieve up to 50% unit cost reductions, rapid prototype iteration, and scalable mass production without compromising quality.
Key Whitepaper Takeaways
- Local Ecosystem Synergy: How Milan’s luxury design legacy intersects with advanced powder metallurgy.
- Economic Benchmarking: Comparative cost & lead-time analysis: MIM vs. 5-Axis CNC Machining vs. Die Casting.
- Metallurgical Precision: Processing 316L, 17-4PH, Titanium Ti-6Al-4V, and Fe-Ni low-alloy steels to >97% theoretical density.
- DFM & Supply Chain Resilience: Leveraging Chinese automated debinding and sintering scale for fast-track European deployment.
- Regulatory & Quality Protocols: Navigating REACH, RoHS, Conflict-Free Minerals, and IATF 16949 compliance for EU entry.
The Milan & Lombardy Industrial Landscape: Sourcing Requirements
Understanding Northern Italy's unique manufacturing matrix—where high fashion, precision mechanics, and smart technology converge.
1. Luxury Wearables & "Lux-Tech"
Milan is recognized globally as the fashion capital, but its tech sector is rapidly expanding into "Lux-Tech." Brands producing premium smartwatches, smart jewelry, and luxury health trackers require metal hardware that fulfills two rigorous criteria: unyielding structural integrity and flawless cosmetic appeal. Chinese MIM allows complex organic curves, micro-engraved branding, and PVD-ready surfaces for 316L and Titanium components.
2. High-End Audio & Wearable Acoustics
The Lombardy regional industrial network houses world-class acoustic engineering firms and boutique consumer audio brands. Custom earphone sound chambers, acoustic nozzles, and wireless earbud hinges require acoustic damping properties and intricate internal cavities that cannot be economically machined via traditional turning. MIM provides internal acoustic paths with zero parting line flash.
3. Smart Home & Industrial IoT Modules
From automated building controls in Milan's modern business districts to high-precision sensors deployed across Northern Italy’s industrial automation belt, demand for compact, durable metal enclosures, internal micro-gears, and latching mechanisms has surged. MIM delivers high magnetic permeability metals and wear-resistant structural parts at massive annual scale.
Engineering Comparison: Manufacturing Processes for Electronics
Why leading global hardware procurement managers choose MIM over conventional metalworking methods.
| Manufacturing Process | Geometric Complexity | Material Utilization | Unit Cost (High Volume) | Surface Roughness (Ra) | Mechanical Strength |
|---|---|---|---|---|---|
| Metal Injection Molding (MIM) | Extremely High (3D Shapes) | > 95% (Near-Net-Shape) | Very Low (Highly Efficient) | 1.0 – 1.6 µm (Polishing Ready) | High (>97% Theoretical Density) |
| 5-Axis CNC Machining | Medium to High | 15% – 40% (High Scrap) | Extremely High (Tooling Wear) | 0.4 – 0.8 µm | Wrought Properties (100%) |
| Aluminum / Zinc Die Casting | High (Thin Wall Limits) | 85% – 90% | Low | 1.6 – 3.2 µm | Moderate (Porosity Issues) |
| Conventional Powder Metallurgy | Low to Moderate (2.5D) | > 90% | Very Low | 2.0 – 4.0 µm | Moderate (85-92% Density) |
Why Chinese MIM Factories Outperform European Alternatives
For Milanese electronics firms, sourcing metal parts from specialized Chinese MIM hubs like Ningbo Jiehuang (JHMIM) provides critical structural benefits that extend far beyond baseline labor savings:
1. Fully Integrated Supply Chain Ecosystems
Our Ningbo manufacturing base consolidates custom feedstock formulation, tooling design & fabrication, catalytic debinding, continuous vacuum sintering furnaces, CNC secondary finishing, and PVD/electroplating within a 30-kilometer radius. This extreme industrial density reduces production lead times by up to 40% compared to fragmented European supply chains.
2. Capital Expenditure & Tooling Amortization
MIM mold design requires highly complex multi-cavity hot runner systems to accommodate linear sintering shrinkage (typically 15-20%). While European tooling shops charge upwards of €25,000 to €50,000 per mold set, Chinese tooling engineering teams construct precision hardened-steel molds at 30-50% of the cost, making mid-to-high volume production viable for fast-moving consumer electronics.
3. Automated Debinding & High-Temperature Sintering Capacity
JHMIM operates advanced continuous atmosphere furnaces (Hydrogen/Nitrogen) capable of precise thermal profiling up to 1380°C. This ensures consistent carbon control, zero distortion, and exceptional batch-to-batch metallurgical repeatability across production runs exceeding millions of pieces per year.
The JHMIM Process Excellence Workflow
Simulation of feedstock flow, mold fill, gate location, and thermal shrinkage within 48 hours of drawing receipt.
Blending ultra-fine elemental metal powders (4-10 µm) with polymer binder systems for optimal flow and green strength.
High-speed automated molding machines shaping complex green parts with intricate internal features and thin walls.
Catalytic debinding followed by solid-state sintering to yield dense, homogenous, high-strength metal components.
Optional CNC coining, magnetic polishing, PVD coating, and 100% CMM dimensional verification before shipment.
Custom Electronics Applications for the Milan Market
Proven engineering solutions tailored to Northern Italy's key technology segments.
Smartwatch Cases & Bezel Frames
MIM 316L and 17-4PH alloys provide high hardness, corrosion resistance, and hypoallergenic properties for wearable technology. Complex internal sealing grooves allow IP68 water resistance while external surfaces accept mirror polishing and PVD rose gold or matte black coatings.
Foldable Smartphone Hinges
Next-generation mobile devices require micro-gear systems and multi-link mechanical hinges capable of undergoing over 200,000 fold cycles. MIM allows high-yield production of ultra-small gears and structural arms with tensile strength exceeding 1100 MPa.
TWS Earbud Acoustic Cavities
High-resolution earphone acoustic chambers require rigid metal bodies to prevent harmonic resonance. MIM titanium and stainless steel parts provide exceptional acoustic dampening in complex thin-walled hollow forms impossible to produce via conventional casting.
Eyewear Hinge Mechanisms
Combining Italy's eyewear heritage with smart eyewear technology. Integrated micro-hinges housing flex cables and sensors are manufactured via MIM in high-strength titanium or nickel-free stainless steel for seamless frame integration.
Connector Enclosures & Type-C Shells
Robust, wear-resistant metal shells for waterproof USB-C connectors, magnetic charging docks, and industrial sensor plugs deployed in harsh operating environments across European automated facilities.
Miniature Thermal Dissipators
Sintered copper and high-conductivity metal alloy heat sinks featuring ultra-dense micro-fin arrays for compact electronic devices, drone controllers, and automotive ECU power modules.
Meeting European Regulatory & Environmental Quality Compliance
Procurement directors and quality managers in Milan and the EU demand strict compliance with international manufacturing, environmental, and ethical standards. JHMIM integrates comprehensive quality assurance protocols into every step of production:
- IATF 16949 & ISO 9001 Certification: Audited quality management systems ensuring full lot traceability, SPC statistical process control, and zero-defect quality initiatives.
- REACH & RoHS Compliance: All raw metal powders, binder formulations, and surface treatments strictly comply with European Union chemical directives (SVHC-free).
- Conflict-Free Mineral Sourcing: Full supply chain verification ensuring raw materials (Nickel, Cobalt, Iron, Titanium) are ethically sourced under global ESG guidelines.
- Strict IP & NDA Protection: Dedicated secure servers, partitioned CAD file access, and legally binding Non-Disclosure Agreements to safeguard proprietary Italian designs.
Sourcing Inspection Matrix
Our quality assurance laboratory utilizes state-of-the-art testing equipment imported from Japan and Germany:
Explore Our Full Range of Precision MIM & Metal Components
Integrated metalworking capabilities spanning MIM, Powder Metallurgy, CNC, and Precision Die Casting.

China Metal MIM Product For Earphone Parts Suppliers & Factories (Milan Audio Spec)
Ultra-precise acoustic housings, sound nozzles, and earbud rotational hinges produced in 316L stainless steel for premium audio brands.
View Product Details
China Custom Precision CNC Machining & Die Casting Aluminum Spare Parts (Milan Auto Supply)
Multi-axis CNC turning and aluminum alloy casting for high-load automotive sensor brackets and industrial machinery components in Lombardy.
View Product Details
Wholesale Customized MIM Injection Molds & High-Precision Aviation Components
In-house hardened steel mold design combined with high-density MIM alloy sintering for aerospace, high-end consumer, and robotics applications.
View Product Details
Wholesale OEM Anodizing Aluminum & Zinc Alloy Die Casting Parts (Milan Enclosures)
Thin-wall aluminum housings and zinc structural brackets finished with decorative anodizing or electroplating for European consumer gadgets.
View Product Details
China Metal Injection Molding Stainless Steel Parts Manufacturers (Milan Tech Hardware)
Mass-produced structural levers, internal lock tabs, and micro-switch components in 17-4PH stainless steel engineered for high fatigue life.
View Product Details
Aluminium Alloy Die Casting with Precision CNC Machining (Milan Hardware Series)
Integrated die-casting and 5-axis CNC finishing services providing high-precision aluminum heat sinks, motor housings, and electronic chassis.
View Product Details
Wholesale Custom MIM Surgical & Micro Hardware Handles Supplier (Precision Ergonomics)
Biocompatible stainless steel and titanium micro-handles featuring knurled anti-slip textures and complex internal assembly geometries.
View Product Details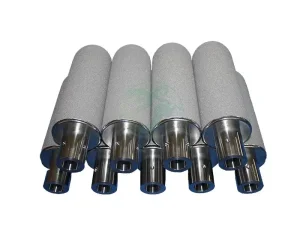
China Sintered Metal Filter Elements Manufacturer (Milan Industrial Filtration Spec)
Porous sintered bronze and stainless steel filter discs providing precise micron rating control for fluid, gas, and acoustic venting systems.
View Product DetailsFrequently Asked Questions: MIM Sourcing for Milan Buyers
Detailed technical insights answering the most critical engineering and procurement inquiries.
What are the standard dimensional tolerances achievable with JHMIM components?
Our standard MIM process achieves dimensional tolerances of ±0.3% to ±0.5% of nominal dimensions without secondary machining (e.g., ±0.03mm on a 10mm feature). For critical fitting dimensions—such as smartwatch bearing pivots or SIM card ejector channels—secondary CNC sizing or micro-coining can tighten tolerances down to ±0.005mm.
Why is MIM more cost-effective than 5-axis CNC machining for complex electronics parts?
5-axis CNC machining removes metal from solid billet stock, resulting in high material waste (often 70-80% scrap), prolonged cycle times (15-45 minutes per part), and rapid cutting tool wear. MIM molds net-shape parts in seconds using a reusable injection tool. Material utilization exceeds 95%, and unit production costs drop dramatically once annual volumes cross 2,000 to 5,000 pieces.
Which stainless steel and metal alloys are best suited for consumer electronics in Milan?
316L Stainless Steel is preferred for smartwatches, earphone nozzles, and wear-adjacent parts due to its superior corrosion resistance and non-allergenic properties. 17-4PH Stainless Steel is chosen for high-stress structural hinges, internal gears, and micro-latches requiring tensile strength up to 1150 MPa. Titanium (Ti-6Al-4V) is increasingly specified for ultra-lightweight luxury wearables.
How does JHMIM manage linear shrinkage during the debinding and sintering process?
During sintering, the removal of polymer binders causes green parts to shrink uniformly by 15% to 20% to reach full theoretical density (>97.5%). Our engineering team uses advanced mold flow and thermal shrinkage simulation software to scale injection mold dimensions precisely. Coupled with continuous atmosphere-controlled sintering furnaces, we maintain tight lot-to-lot consistency.
Can JHMIM support rapid prototyping before we commit to high-volume tooling?
Yes. We provide quick-turn prototyping services using Direct Metal Laser Sintering (DMLS / Metal 3D Printing) or high-speed 5-axis CNC machining in identical metal alloys (316L, 17-4PH, Titanium). This allows Milan design engineers to verify mechanical fit, ergonomics, and aesthetic scale before finalizing MIM production tooling.
What surface finish options are available for cosmetic metal components?
As-sintered MIM components have a surface roughness of Ra 1.0–1.6 µm. We offer a full range of secondary surface finishing processes, including centrifugal barrel tumbling, magnetic bead polishing, high-gloss mirror polishing, sandblasting, PVD (Physical Vapor Deposition) coating in Gold/Rose Gold/Black/Titanium, electroplating, and laser engraving.
What are the typical lead times for tooling development and first sample delivery to Italy?
Standard tooling design and mold fabrication take approximately 25 to 30 days. First Article Inspection (FAI) samples are sintered, measured, and shipped via express air freight (DHL/FedEx) within 3 to 5 days, reaching Milan engineering teams in under 35 days from project approval.
How does JHMIM ensure IP protection for Italian luxury and consumer tech designs?
We adhere to strict confidentiality protocols. Non-Disclosure Agreements (NDAs) are signed prior to drawing submission. Project CAD data is stored on encrypted, access-restricted internal networks, and physical parts are processed under blind batch tracking to prevent unauthorized duplication.
Accelerate Your Consumer Electronics Hardware Development
Partner with Ningbo Jiehuang (JHMIM) for high-precision Metal Injection Molding solutions engineered specifically for Milan’s innovative industrial market. Receive an engineer-reviewed DFM analysis and transparent quotation within 48 hours.
Direct Engineering Contact: [email protected] | WhatsApp: +86 136 0574 5108 | ISO 9001 & IATF 16949 Certified