
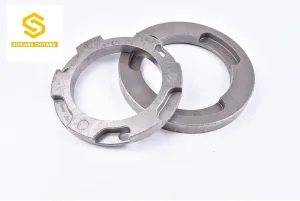






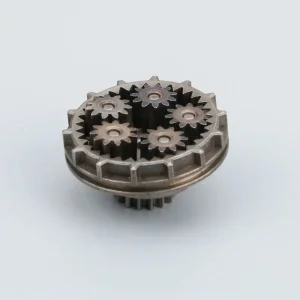
Global Industrial Landscape of Fn-0205 Structural Parts
In modern powder metallurgy (PM) engineering, FN-0205 (Iron-Nickel Steel) represents one of the most widely adopted structural material standards established by the Metal Powder Industries Federation (MPIF Standard 35) and ISO 5755. Engineered specifically for high-load, shock-resistant dynamic mechanical systems, Fn-0205 sintered metal parts offer an exceptional combination of tensile strength, ductility, and fatigue endurance. As global OEM manufacturers transition away from energy-intensive subtractive machining toward near-net-shape sustainable metal forming, China has emerged as the premier global manufacturing hub for Fn-0205 structural components.
High Torque & Fatigue Strength
The addition of 1.5% to 2.5% elemental nickel in the Fn-0205 alloy matrix solid-solves into the iron lattice, significantly inhibiting crack propagation and enhancing microstructural toughness under cyclic dynamic stress loading.
Dimensional Stability
Through precision closed-die compaction and controlled-atmosphere sintering, Fn-0205 parts achieve repeatable IT8-IT10 tolerances straight out of the furnace, virtually eliminating expensive secondary CNC hobbing or milling operations.
Heat Treatment Response
Fn-0205 exhibits remarkable hardenability. Post-sintering carbonitriding, case hardening, or oil quenching transforms the mixed pearlite-ferrite microstructure into high-hardness tempered martensite exceeding 35-45 HRC.
Metallurgical Specifications & Mechanical Properties Matrix
Understanding the microstructural mechanics of Fn-0205 requires evaluating chemical stoichiometry, compaction pressure, sintering furnace kinetics, and density gradients. As a trusted China Fn-0205 structural parts manufacturer, our facilities operate under rigid ISO 9001:2015 and IATF 16949 quality systems.
| Property Parameter | As-Sintered (6.8 g/cm³) | High Density (7.2 g/cm³) | Heat Treated (HT / Case Hardened) | Testing Standard |
|---|---|---|---|---|
| Chemical Composition | Fe: Balance | Ni: 1.5 - 2.5% | C: 0.4 - 0.7% | Other Elements < 2.0% max | MPIF Standard 35 / ISO 5755 | ||
| Ultimate Tensile Strength (UTS) | 320 - 380 MPa | 480 - 560 MPa | 750 - 900 MPa | ASTM E8M / ISO 2740 |
| Yield Strength (0.2% Offset) | 220 - 260 MPa | 340 - 410 MPa | 620 - 750 MPa | ASTM E8M |
| Apparent Hardness | 60 - 75 HRB | 75 - 90 HRB | 32 - 45 HRC | ASTM E18 / ISO 4498 |
| Impact Energy (Charpy Unnotched) | 12 J | 25 J | 16 J | MPIF Standard 40 |
| Fatigue Limit (S-N Curve) | 140 MPa | 210 MPa | 310 MPa | MPIF Standard 56 |
| Elongation (in 25mm) | 2.0% | 4.5% | < 1.0% | ASTM E8M |
Where Fn-0205 Structural Parts Drive Global Innovation
From heavy-duty industrial planetary gearboxes to precision automotive engine actuators, Fn-0205 structural parts manufactured in China serve as core load-bearing components across high-tier global manufacturing sectors.
Automotive Powertrain
Engine timing sprockets, variable valve timing (VVT) rotors, oil pump gears, transmission sync hubs, and seat adjuster gear segments requiring strict dynamic fatigue resistance.
Professional Power Tools
High-impact bevel gears, planetary gear carriers, impact wrench anvils, and cordless hammer drill gearboxes operating under high shock loading and intermittent friction.
Hydraulics & Fluid Power
Gerotor fuel pump gears, hydraulic motor valve plates, distributor sleeves, and high-pressure fluid metering gears demanding minimal internal porosity leakage.
Industrial Machinery
Heavy-duty bushings, lock hardware mechanisms, textile machine cams, agricultural harvester drive hubs, and robotic joint actuators engineered for extended operational life.
How China Facilities Achieve Microstructural Superiority
Producing high-grade Fn-0205 sintered parts requires rigorous control over elemental powder atomization, solid-state press kinetics, sintering atmosphere equilibrium, and post-sintering secondary processing.
1. Powder Homogenization
Water-atomized high-purity iron powder is blended with carbonyl nickel powder (1.5–2.5%), synthetic graphite (0.4–0.7%), and organic lubricants (zinc stearate or Acrawax). High-efficiency double-cone blenders ensure zero segregation prior to compaction.
2. Multi-Ram CNC Compaction
Using advanced 100 to 1,000-ton automated hydraulic and mechanical powder presses, the alloy mixture is compacted at pressures ranging from 400 to 700 MPa to produce "green" compacts with precise structural density (6.8 – 7.2 g/cm³).
3. High-Temp Belt Sintering
Green compacts travel through continuous mesh-belt furnaces at 1120°C to 1150°C under a protective endothermic or synthetic Nitrogen-Hydrogen (90/10) reducing atmosphere, facilitating atomic diffusion of nickel into the iron lattice.
4. Rapid Sinter-Hardening
Equipped with convective fast-cooling zones in sintering furnaces, the parts undergo controlled cooling rates exceeding 2°C/sec, directly transforming the austenite matrix into high-strength martensite/bainite without oil quenching distortional risks.
5. Precision Sizing & Repressing
For ultra-tight dimensional specifications (such as ISO Class 7 gear teeth), sintered components undergo coining, sizing, or repressing in dedicated sizing dies to eliminate sintering shrinkage variations and optimize radial surface finish.
6. Oil Impregnation & Coating
Interconnected surface pores are vacuum-impregnated with synthetic rust-inhibiting lubricants or resin sealed prior to secondary electroplating (zinc, nickel, black oxide) or steam treatment for enhanced corrosion protection.
Why Sourcing Fn-0205 Parts from China Delivers Unmatched ROI
China’s mature powder metallurgy industrial ecosystem offers international procurement managers and lead design engineers unparalleled economic and technical efficiency.
Vertical Powder Atomization Integration
Direct access to China’s major raw material atomization foundries eliminates long lead times and international freight surcharges for specialized Fe-Ni master powders, keeping base material costs highly competitive.
In-House High-Precision Tooling Fabrication
Equipped with slow-wire EDM, mirror-finish EDM, and CNC jig grinders, Chinese PM suppliers design and manufacture ultra-hard tungsten carbide dies in-house within 3 to 4 weeks at a fraction of Western tooling costs.
Comprehensive Testing Infrastructure
Leading China suppliers maintain dedicated quality control laboratories outfitted with Zeiss CMMs, CSEM micro-indentation hardness testers, Oxford X-ray fluorescence spectrometers, and density evaluation balances.
Global OEM Procurement & Risk Mitigation Protocol
When procuring Fn-0205 structural parts internationally, engineering teams must evaluate specific quality control milestones to guarantee seamless batch-to-batch consistency and assembly line compatibility.
1. Design for Manufacturability (DFM)
Ensure drawings incorporate appropriate punch land widths (>0.8mm), avoid razor-thin wall sections (<1.5mm), provide 10° to 15° chamfers to assist tool ejection, and optimize feather-edge radii to prevent tool chipping.
2. PPAP Level 3 Documentation
Insist on complete Production Part Approval Process deliverables, including Process Flow Diagrams, Process Failure Mode and Effects Analysis (PFMEA), Control Plans, Gauge R&R studies, and Full Dimensional Inspection Reports.
3. Microstructural & Density Audits
Verify that the supplier conducts Archimedes method density testing across cross-sectional zones to ensure uniform density distribution, preventing localized soft spots or premature fatigue cracking under shear stress.
Technological Innovations Driving Next-Gen Sintered Steel
The powder metallurgy industry is evolving rapidly. Advanced China factories are integrating artificial intelligence, warm compaction techniques, and hybrid manufacturing to expand the physical capabilities of Fn-0205 structural components.
Warm Compaction & Heated Dies
By heating both the organic polymer-lubricated Fn-0205 powder mixture and the carbide die cavity to 130°C–150°C, single-press compaction achieves green densities up to 7.35 g/cm³ without requiring double-press double-sinter (DPDS) processing.
AI Closed-Loop Sintering
Real-time infrared camera sensors and mass spectrometer gas analyzers feed carbon potential and temperature micro-fluctuations directly into AI control algorithms, preserving precise carbon stoichiometry across 24/7 continuous furnace runs.
Surface Rolling & Localized Densification
Applying specialized CNC roller-burnishing to critical gear tooth flanks cold-works the surface layer of Fn-0205 gears to near 100% theoretical density (7.8 g/cm³), unlocking extreme bending fatigue resistance comparable to forged steel.
Frequently Asked Questions: Fn-0205 Manufacturing & Procurement
Direct answers to critical technical questions asked by global design engineers and procurement managers sourcing Fn-0205 structural parts from China.





