
Featured Aerospace & Precision Powder Metallurgy Solutions
Explore our primary qualified product inventory engineered for high-stress aerospace actuations, high-temperature MIM processing, and precision powertrain applications.






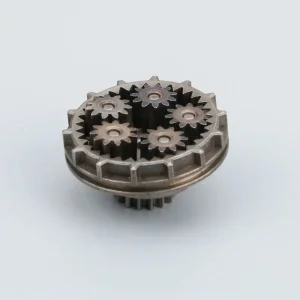

Aerospace Gearing Architecture: Engineering Beyond Conventional Limits
Modern aerospace propulsion, flight control, and auxiliary systems demand gear units capable of transferring extreme torque under severe vibration, thermal shocks (-65°C to +450°C), and uncompromising weight restrictions.
As a premier wholesale aerospace gear manufacturer and custom powder metallurgy supplier, Ningbo Jiehuang Chiyang Electronic Tech Co., Ltd. (JHMIM) bridges the gap between ultra-precision mechanical engineering and scalable smart manufacturing. Precision aerospace gears are not merely mechanical power transmission elements; they are mission-critical components where a micro-scale surface flaw can result in catastrophic system fatigue. From AGMA Quality Class 11 to Class 15 precision standards, our manufacturing workflows utilize Advanced Metal Injection Molding (MIM), Hot Isostatic Pressing (HIP), 5-axis CNC gear generating grinding, and high-density powder metallurgy (PM) synthesis to yield unprecedented power-to-weight ratios.
By integrating specialized flight-grade alloys such as Pyrowear 53, Ferrium C64, 17-4PH stainless steel, and Titanium Ti-6Al-4V into net-shape production processes, we enable aerospace Tier-1 and OEM engineers to bypass conventional machining bottlenecks. This guide details our technical roadmap, compliance frameworks, near-net-shape metallurgy cost dynamics, and strategic procurement advantages for next-generation aviation networks.
Aerospace Gear Technology Roadmap & Future Outlook
Next-generation aviation architectures—spanning Hybrid-Electric Aircraft, Urban Air Mobility (eVTOL), Deep-Space Probes, and Hypersonic Actuators—demand a fundamental paradigm shift in gear metallurgy and tooth profile synthesis.
High-Density MIM + HIP Gearing
Combining precision Metal Injection Molding with secondary Hot Isostatic Pressing (HIP) eliminates residual micro-porosity. This achieves near 100% density, matching wrought material fatigue strength while reducing complex geometry production costs by up to 48%.
Asymmetric Tooth Modifications
Custom pressure angles (e.g., 25° drive side / 15° coast side) optimized via AI finite element analysis (FEA). This increases drive-side root bending strength by 35% without increasing envelope weight.
Nanocomposite PVD Coatings
Application of DLC (Diamond-Like Carbon), TiAlN, and Balinit C coatings to gears operated in dry or boundary-lubricated environments, ensuring scuffing resistance under extreme high-speed conditions.
Macro Industry Engineering Solutions
JHMIM customizes gear kinematics, surface metallurgy, and quality validation specifically aligned with high-tier aerospace applications.
Commercial Aviation Turbofans & APUs
Auxiliary gearbox (AGB) planetary systems, fuel pump drives, and starter gear trains operating continuously under high oil temperatures. We utilize vacuum-carburized low-alloy steels and specialized bronze-powder sintered sleeves to guarantee low NVH and over 30,000 flight hours mean time between failures (MTBF).
Defense & Missile Guidance Actuation
High-density zero-backlash spur and harmonic gear drives for fin controls, radar tracking gimbals, and target acquisition systems. Manufactured via MIM 17-4PH and Titanium sintering, providing ultra-compact form factors capable of sustaining shock loads up to 100G.
eVTOL & Electric Propulsion Drives
Ultra-lightweight gearboxes designed for high-RPM electric motors in Urban Air Mobility craft. High surface-hardness teeth with optimized crown-ground profiles drastically minimize high-frequency acoustic signatures while maintaining structural safety margins.
China Industry 4.0: Supply Chain Resilience & Cost/Efficiency Advantages
Integrating modern smart manufacturing into powder metallurgy and gear grinding redefines high-precision gear sourcing economics for international OEMs.
Near-Net-Shape MIM Efficiency
Traditional aerospace gear production machines away up to 80% of expensive raw material forged bars. Our automated Metal Injection Molding (MIM) process achieves over 95% material utilization, yielding massive unit cost reductions for high-alloy stainless and titanium components.
Digital Twin & Closed-Loop Sintering
Our continuous atmosphere-controlled sintering furnaces utilize real-time thermal sensors and digital twin simulations to control mold shrinkage precisely. This achieves batch-to-batch repeatability within ±0.03mm prior to final gear tooth grinding.
Full Supply Chain Synergy
From internal tooling fabrication, powder synthesis, and compaction pressing to CNC tooth profile grinding and localized PVD coating, JHMIM keeps 100% of critical manufacturing steps in-house. This guarantees rapid prototyping lead times (30 days vs 120 days industry average).
Aerospace Gear Material & Manufacturing Matrix
A detailed technical comparison of precision metallurgy routes for high-stress aerospace power transmission.
| Manufacturing Process | Primary Material Standard | Achievable Density | AGMA Precision Level | Surface Fatigue Limit (MPa) | Cost Benefit vs CNC |
|---|---|---|---|---|---|
| MIM + HIP Process | 17-4PH / Ti-6Al-4V / 316L | 99.5% - 99.8% | AGMA Class 8 - 11 | 1,250 MPa | 40% - 55% Lower |
| High-Density PM Pressing | MPIF 35 / Fe-Ni-Cu Steel | 92.0% - 95.5% | AGMA Class 7 - 9 | 950 MPa | 50% - 65% Lower |
| PM Gear + Precision Grinding | Pyrowear 53 / Ferrium C64 | 98.5% - 99.2% | AGMA Class 12 - 14 | 1,650 MPa | 25% - 35% Lower |
| Conventional Machining | Wrought Aerospace Bar stock | 100% | AGMA Class 10 - 15 | 1,700 MPa | Baseline High Cost |
Localization Support & Compliance Safeguards
We eliminate international sourcing risks through strict compliance protocols, transparent quality documentation, and global technical support.
Regulatory Compliance
Operated under ISO 9001:2015 and IATF 16949 certified quality management systems. Fully aligned with REACH, RoHS, and international raw material melt source traceability standards.
Non-Destructive Testing (NDT)
100% inspection capabilities including CMM 3D scanning, magnetic particle inspection (MPI), ultrasonic flaw detection, and micro-hardness profile mapping across gear tooth roots.
IP Protection & NDA Architecture
Strict legal non-disclosure frameworks protecting customer STEP models, print drawings, and proprietary alloy specifications under isolated server infrastructure.
Global Enterprise Procurement & Sourcing Management
Optimizing Total Cost of Ownership (TCO) through engineering-led procurement partnerships.
When procuring wholesale aerospace gear systems and sintered components, enterprise procurement directors must balance unit economics with stringent reliability thresholds. Standard low-cost sourcing often risks high defect rates or extended lead times. JHMIM mitigates supply chain vulnerability through dedicated account engineering management, complimentary DFM reviews on every drawing, transparent pricing itemization, and dual-facility logistics redundancy in Ningbo, China.
Accelerate Your Aerospace Gear Procurement
Submit your 2D PDF & 3D STEP files today. Receive a complete engineering DFM feasibility assessment and itemized commercial quote within 48 hours.
Connect with Senior Gear SpecialistsFrequently Asked Questions (Technical & Commercial FAQ)
In-depth responses to critical engineering and purchasing inquiries regarding aerospace gearing and MIM component fabrication.
Metal Injection Molding (MIM) excels at producing small, highly intricate gear geometries (such as internal splines, dual-gear clusters, and lightweight structural cutouts) directly in net-shape form without multi-axis machining. While traditional gear hobbing removes material from solid bar stock, MIM molds net shapes with over 95% material utilization. When combined with Hot Isostatic Pressing (HIP) and final tooth grinding, MIM gears achieve comparable density and strength at significantly lower mass-production costs.
Through near-net-shape powder metallurgy and sintering alone, we consistently achieve AGMA Class 7 to Class 9. For flight-critical aerospace applications requiring high precision, we integrate secondary CNC tooth generating grinding and micro-honing, delivering gear tolerances up to AGMA Class 14 (ISO 3/4 standards).
We regularly process high-performance aerospace alloys including 17-4PH stainless steel, 316L, Titanium (Ti-6Al-4V), Fe-Ni-Cu low-alloy steels, Molybdenum alloys, and bronze sintering powders. Customized powder formulations can also be engineered to match specific thermal expansion or magnetic requirements.
Tooling development and initial sample validation (supported by FAI inspection reports) typically take 30 days. Metal 3D-printed prototype samples can be provided within 7 days for early functional testing before committing to mold tooling. Production lead times average 3 to 4 weeks depending on order volume and required surface treatments.
Every production run undergoes strict quality gates under ISO 9001 and IATF 16949 systems. We employ over 30 dedicated Quality Control specialists, utilizing CMMs, optical profile projectors, spectrum analyzers, and density testers. 100% critical dimension checks are conducted prior to dispatch, and all shipments carry a 1-year product quality warranty.
Additional Custom Precision Components & Assemblies
Browse our expanded line of precision MIM, sintered bushings, structural connectors, and custom hardware.






