
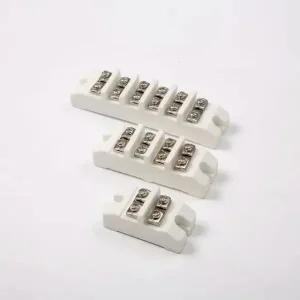

Wholesale Professional Factory for Wholesale Motorcycle Accessories Aluminum Alloy Part Motorcycle Windscreen Die Casting Supplier, Factories
View Details
Wholesale OEM Factory for Customized Phone Button Watch Button by MIM Metal Injection Molding Factory, Factories
View Details
Wholesale Hot-selling China Pm Powder Metallurgy Sintering Parts Manufacturers, Supplier
View Details

China Super Lowest Price Powder Metallurgy Micro Precision Machining for Auto Metal Truck Stainless Stee Accessory Auto Parts by MIM Suppliers, Factories
View Details
China China OEM MIM Auto Spare Parts Car Parts Accessories Motor Motorcycle Parts by Metal Injection Molding CNC Machining Suppliers, Factories
View Details
Wholesale Good Wholesale Vendors Factory Custom MIM Metal Injection Molding MIM Gear Part for Electronic Components Manufacturer, Manufacturers
View DetailsState of Powder Metallurgy & MIM Technology
The global powder metallurgy industry is undergoing a paradigm shift toward ultra-high density, complex net-shape geometries, and multi-material alloy formulations. As a Tier-1 OEM/ODM manufacturer in China, Jiehuang (JHMIM) delivers end-to-end engineered powder metal solutions that replace traditional subtractive CNC machining while drastically lowering unit costs.
Metal Injection Molding (MIM)
MIM combines the design flexibility of plastic injection molding with the mechanical integrity of wrought metals. By blending micron-sized spherical metal powders with thermoplastic binders, our automated vacuum debinding and high-temperature sintering processes produce complex 3D micro-structural parts with high tensile strength and dynamic fatigue limits.
Press-and-Sinter Metallurgy (PM)
Utilizing high-tonnage automated compaction presses (up to 1,000 tons / 10,000 kN), we produce structural planetary gears, timing pulleys, and self-lubricating bearings. Conforming strictly to MPIF Standard 35 and ASTM standards, PM technology offers unmatched dimensional stability for high-volume automotive and industrial gearboxes.
Spherical Powders & Titanium MIM
We process ultra-pure spherical gas-atomized metal powders including Ti-6Al-4V, Ti45Al8Nb titanium aluminides, 17-4PH, 316L stainless steel, and Fe-Ni low alloy powders. Our materials exhibit low brittleness, high plasticity, and superior corrosion resistance for medical devices and aerospace structural components.
China Manufacturing Advantage: Ningbo Precision Hub
Located in the Yangtze River Delta manufacturing ecosystem of Ningbo, China, Ningbo Jiehuang Chiyang Electronic Tech Co., Ltd. (JHMIM) provides global buyers with an integrated end-to-end production pipeline from raw material synthesis to CNC post-machining and surface treatment.
In-House Tooling & DFM Review
Our engineering team conducts a complete Design for Manufacturability (DFM) review within 48 hours for every technical drawing submitted. With complete control over mold flow analysis, shrinkage factor calculation (typically 15-20% linear shrinkage during sintering), and multi-cavity tool build, we cut prototype lead times by 40%.
Rigorous QA & Metallurgical Control
Operating under ISO 9001 and IATF 16949 certified quality systems, our laboratory features Zeiss Coordinate Measuring Machines (CMM), optical profile projectors, carbon-sulfur analyzers, and inductively coupled plasma (ICP) spectrometers to guarantee batch-to-batch chemical and dimensional consistency.
Optimized Landed Supply Chain Cost
By leveraging domestic raw material supply chains for high-purity iron, nickel, stainless steel, and titanium powders, we offer global procurement teams transparent pricing. Save significantly on component unit prices without compromising microstructural strength or tolerance specs.
E-E-A-T Engineering Note: Vacuum sintering at JHMIM is conducted under partial pressures of argon or hydrogen atmospheres at temperatures up to 1380°C (2516°F). This achieves near-wrought density (>98%) and eliminates interconnected porosity, allowing components to be electroplated, PVD-coated, or heat-treated (carburizing, nitriding, induction hardening) without salt trap risks.
Engineering Matrix: Selecting the Right Manufacturing Technology
Choosing the proper metal forming process requires balancing geometric complexity, production volume, material selection, and target tolerances. The comparison table below highlights why Metal Injection Molding (MIM) and Powder Metallurgy (PM) outperform legacy metalworking processes for high-volume parts.
| Manufacturing Process | Geometric Complexity | Dimensional Tolerance | Material Density | Economic Volume (MOQ) | Machining Waste |
|---|---|---|---|---|---|
| Metal Injection Molding (MIM) | Ultra-High (Undercuts, 3D Curves, Micro Holes) | ±0.3% to ±0.5% (±0.05 mm) | 95% – 99% | 2,000 + pcs | Near-Zero (< 2%) |
| Powder Metallurgy (PM Press & Sinter) | Medium (2.5D Stepped Geometries, Gears) | ±0.1% to ±0.3% | 85% – 92% (Up to 95% re-pressed) | 5,000 + pcs | Near-Zero (< 1%) |
| Aluminum / Zinc Die Casting | High (Thin-walled Housings, Cavities) | ±0.1 mm | Cast Density (Porosity potential) | 2,000 + pcs | Low (Sprues recycled) |
| CNC Subtractive Machining | Moderate to High (Limited by tool access) | ±0.005 mm – ±0.02 mm | 100% (Wrought Bar Stock) | 1 – 500 pcs | High (Up to 70% scrap) |
| Metal 3D Printing (SLM/DMLS) | Maximum (Internal Channels, Lattice) | ±0.1 mm | 99%+ | 1 – 100 pcs (Prototyping) | Low |
Global Industry Solutions & Localized Applications
JHMIM metal powder components serve mission-critical applications across global markets. Our micro-precision metal parts meet strict engineering standards across five primary industrial sectors.
Automotive & Electric Vehicles (EV)
We manufacture IATF 16949 compliant components including Variable Valve Timing (VVT) rotors, oil pump gears, seat belt lock pawls, turbocharger vanes, windshield wiper motor gears, and EV battery connector terminals. High fatigue endurance ensures long life cycles under thermal shock and severe vibrational loads.
Medical Devices & Surgical Tools
Using 316L, 17-4PH stainless steel, and Ti6Al4V Titanium alloy powders, we supply biocompatible laparoscopic surgical instrument jaws, titanium scalpel handles, endoscopic stapler components, and MIM orthodontic brackets. Surface roughness can be electro-polished to mirror finish Ra < 0.2 µm.
Consumer Electronics & Wearables
As smart devices shrink in size, traditional micro-machining reaches its economic limit. JHMIM mass-produces micro foldable phone screen hinges, smartwatch titanium housings, earphone sound chamber structures, phone button actuators, and ceramic terminal connectors with micro-wall thicknesses down to 0.3 mm.
Power Tools & Industrial Hardware
For high-torque hand tools, pneumatic tools, and lock hardware, PM press-and-sinter technologies provide high strength-to-weight ratios. We engineer heavy-duty planetary gear carriers, impact wrench ratchets, lock cylinders, and wear-resistant tungsten carbide matrix parts.
Material Science: Alloy Engineering Datasheet
Our powder metallurgy engineers formulate raw powder feeds in-house to tailor mechanical properties including yield strength, elongation, hardness, and wear resistance to exact customer requirements.
| Material Designation | Equivalent Grade | Tensile Strength (MPa) | Yield Strength (MPa) | Elongation (%) | Hardness (As Sintered / Heat Treated) |
|---|---|---|---|---|---|
| MIM 17-4PH | ASTM A564 (AISI 630) | 1,150 – 1,300 | 1,000 – 1,150 | 4% – 6% | 35 – 42 HRC (H900 Condition) |
| MIM 316L | ASTM A240 (AISI 316L) | 520 – 600 | 200 – 250 | 40% – 50% | 65 – 75 HRB (Austenitic Non-Magnetic) |
| MIM 4605 (Fe-Ni-Mo) | Low Alloy High Strength Steel | 1,450 – 1,650 | 1,250 – 1,400 | 2% – 4% | 45 – 52 HRC (Quenched & Tempered) |
| TiMIM Ti-6Al-4V | ASTM B348 Grade 5 | 880 – 950 | 800 – 860 | 10% – 15% | 30 – 36 HRC (Biocompatible, Lightweight) |
| PM FN-0205 | MPIF 35 Sintered Iron-Nickel | 400 – 650 | 280 – 450 | 1.5% – 3% | 65 – 85 HRB (Sinter Hardened) |
| Spherical Ti45Al8Nb | Intermetallic Titanium Aluminide | 650 – 780 | 550 – 620 | 1.0% – 2.0% | High Temp Oxidation Resistant (>700°C) |
Global Procurement Roadmap: How We Work With You
From initial concept and prototype verification to mass production and global shipping, JHMIM provides global procurement managers and design engineers with a transparent 5-step operational workflow.
Step 1: Drawing Review & Non-Disclosure Agreement (NDA)
We execute strict NDA protocols prior to file exchange. Send us your 3D STEP/IGES CAD models along with 2D PDF technical drawings specifying tolerances, critical dimensions (KPC), and surface finishes.
Step 2: Engineering DFM & Transparent Quotation
Within 48 hours, our engineering team submits a comprehensive DFM manufacturability report highlighting gate locations, parting lines, draft angles, ejector pin marks, and shrinkage compensations alongside mold tooling and piece-price quotes.
Step 3: Rapid Prototyping & Mold Construction
To validate form and fit before cutting hard tooling, we supply metal 3D-printed (SLM) prototypes. Upon drawing approval, our CNC EDM toolroom fabricates multi-cavity hardened steel injection molds (H13 / S136, 52-55 HRC).
Step 4: Sample Verification & PPAP Submission
We deliver First Article Samples (T1) backed by full inspection reports: CMM dimensional measurement, density analysis, tensile test reports, and PPAP Level 3 documentation for automotive OEM clients.
Step 5: Automated Mass Production & Global Logistics
Upon approval, we commence mass production with continuous statistical process control (CPK > 1.33). Shipments are vacuum packed with VCI corrosion inhibitors and dispatched by ocean freight, air express, or DDP directly to your warehouse.
Frequently Asked Questions (FAQ)
Common technical and commercial questions from global purchasing directors, mechanical design engineers, and supply chain managers.
Press-and-Sinter Powder Metallurgy (PM) uses uniaxial compaction of coarse powders in a rigid die cavity, restricting shapes to 2.5D geometries with uniform vertical cross-sections. In contrast, Metal Injection Molding (MIM) utilizes micro-fine metal powders mixed with polymer binders to mold intricate 3D shapes with complex undercuts, internal threads, and variable wall thicknesses, achieving much higher relative densities (>96% vs 85-92%).
Yes. We routinely review and sign client NDAs before receiving any proprietary engineering drawings or project files. All CAD data, specifications, and project communications remain strictly confidential under our secure internal data governance system.
Standard standard dimensional tolerances for as-sintered MIM components range from ±0.3% to ±0.5% of the nominal dimension (typically down to ±0.05 mm for small features). For tighter tolerance features (e.g. IT6 to IT7 fits, tight bearing bores under ±0.01 mm), we perform secondary CNC machining, sizing, grinding, or CNC wire EDM in-house.
The 3D model allows our software to calculate component volume, weight, mold flow dynamics, and shrinkage rates. The 2D drawing specifies critical geometric tolerances (GD&T), surface finish requirements (Ra), raw material grade, heat treatment hardness, and electroplating specifications necessary to prepare an accurate quotation.
Our standard MOQ is 2,000 pieces for MIM structural components, 5,000 pieces for press-and-sinter powder metallurgy gears, and 2,000 pieces for aluminum/zinc die casting parts. Prototype quantities and pilot sample runs are provided during the tooling development phase.
After vacuum debinding and high-temperature sintering, MIM parts achieve densities exceeding 96% to 98% of theoretical density. Consequently, their mechanical properties—such as tensile strength, yield strength, impact toughness, and corrosion resistance—are virtually identical (>95%) to wrought metal, while reducing material waste by up to 90% and cost by 30% to 50% for complex volume orders.
Standard lead time for mold design, CNC tooling fabrication, and T1 sample delivery is approximately 30 calendar days. Expedited tooling schedules can be arranged for urgent prototype verification projects using 3D metal printing (SLM).
Because JHMIM sintered components have ultra-high core density without interconnected surface porosity, they readily accept electroplating (nickel, chrome, gold, zinc), physical vapor deposition (PVD), black oxide, passivation, anodizing (for aluminum die casting), sandblasting, laser engraving, and thermal heat treatment (carburizing, nitriding, quenching).

Wholesale Cheap price China &Nbsp; Spherical Ti45al8nb Powder with Good Plasticity and Low Brittleness Manufacturer, Factory
View Details
Wholesale Competitive Price for Powder Metallurgy Auto Parts Good Quality Wiper Motor Part Manufacturer, Manufacturers
View Details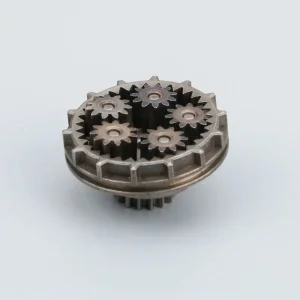
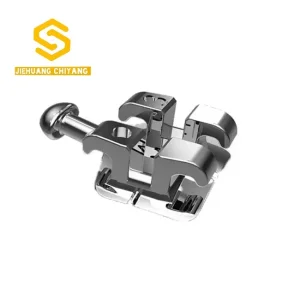
Wholesale dental supplies ortodoncia equipments MIM mesh base metal orthodontic MIM brackets Factory, Factories
View Details
Wholesale Free sample for OEM/ODM High Density Low Alloy Steel/Titanium Powder Metal Injection Molding Electronic Component Manufacturer, Suppliers
View Details
China Professional China China Metal Injection Molding (MIM) Parts for Complex Structural Components Machinery Parts Manufacturers, Factories
View DetailsAccelerate Your Engineering Procurement Today
Send us your 2D/3D CAD drawings (STEP, IGES, PDF). Receive an engineer-reviewed DFM analysis, mold design recommendation, and transparent price quotation within 48 hours.
Request Free DFM & Quote Now