
High-Demand Custom OEM Metals for Dutch Manufacturers
Engineered for seamless integration into Benelux industrial supply chains, adhering to DIN, ISO, and ISO/TS 16949 international benchmarks.




1. Executive Summary: Sourcing Chinese OEM Precision Components in the Netherlands
The Netherlands stands as one of Europe’s premier technological hubs, anchored by world-leading industrial clusters such as Brainport Eindhoven (semiconductor capital equipment and high-tech systems), the Rotterdam Maritime Delta (offshore engineering, shipbuilding, and port machinery), and the growing green-tech and agro-robotics ecosystems in Wageningen and Westland. As Dutch Original Equipment Manufacturers (OEMs) face pressure to accelerate innovation cycles while optimizing total cost of ownership (TCO), cross-border strategic sourcing from specialized Chinese precision engineering manufacturers has shifted from a pure cost-reduction play to a critical competitive capability.
In the current geopolitical and macroeconomic climate, Dutch procurement directors and senior mechanical engineers require partners who not only offer raw cost advantages but also meet rigorous European quality protocols. Sourcing complex components—ranging from high-density Metal Injection Molding (MIM) surgical jaws and automotive actuator gears to large-scale aluminum die-cast electronic housings—demands strict compliance with EU directives including REACH, RoHS, and the Carbon Border Adjustment Mechanism (CBAM).
Ningbo Jiehuang Chiyang Electronic Tech Co., Ltd. (JHMIM) bridges the operational gap between Chinese high-capacity industrial manufacturing and Dutch precision engineering standards. By providing full transparency, rigorous Design for Manufacturability (DFM) reviews, and robust ISO 9001 / IATF 16949 certified quality management, JHMIM empowers OEMs in Amsterdam, Eindhoven, Rotterdam, Utrecht, and Enschede to achieve unmatched manufacturing agility.
2. Advanced Engineering Processes: MIM, PM, Die Casting & CNC
Choosing the optimal manufacturing process for complex metal components requires balancing mechanical stress, geometry, material properties, production volume, and initial tooling investments.
Metal Injection Molding (MIM)
MIM combines the geometric design freedom of plastic injection molding with the structural integrity of wrought metals. By blending ultrafine metal powders with polymer binders, JHMIM produces complex, 3D net-shape parts with densities exceeding 95% to 99% of theoretical values.
- Ideal Materials: 17-4PH, 316L, 4140, Ti-6Al-4V (Titanium), Tungsten.
- Key Applications: Medical surgical handles, lock micro-mechanisms, wearable electronics, automotive sensor mounts.
- Batch Volume: 2,000 to 1,000,000+ pieces/year.
Powder Metallurgy (PM / Sintering)
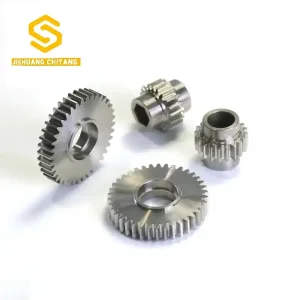
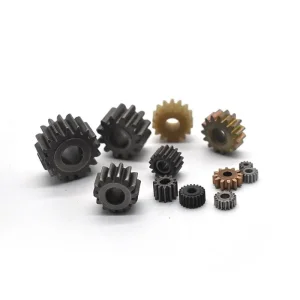
Press-and-sinter powder metallurgy is the most economical solution for high-volume structural components, spur/helical gears, and oil-impregnated self-lubricating bearings. Utilizing 1,000-ton automated compaction presses, JHMIM yields near-zero material waste.
- Standards: MPIF 35, DIN 30910, ISO 5755.
- Key Applications: Planetary gearboxes, electric motor bushings, water pump pulleys, hydraulic valve components.
- Cost Savings: Up to 60% lower unit price vs. multi-axis CNC hobbing.
Aluminum & Zinc Die Casting
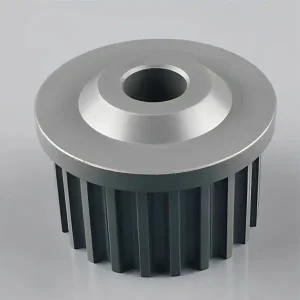
High-Pressure Die Casting (HPDC) provides light-weighting, exceptional thermal conductivity, and structural rigidity for larger enclosures and structural frames. In-house CNC finishing ensures mating surfaces hit sub-hundredth millimeter callouts.
- Alloys Used: ADC12, A380, A356, Zamak 3, Zamak 5.
- Key Applications: E-mobility drive housings, LED heat sinks, optical instrument frames, drone chassis.
- Surface Finishing: Powder coating, anodizing, chromate conversion, e-coating.
Engineering Decision Matrix: MIM vs. Powder Metallurgy vs. Die Casting vs. CNC
This benchmark table aids Dutch engineering leads in determining the right process route prior to locking in final CAD designs.
| Parameter | Metal Injection Molding (MIM) | Powder Metallurgy (PM) | High-Pressure Die Casting | 5-Axis CNC Machining |
|---|---|---|---|---|
| Target Part Weight | 0.2g to 250g (Max 286g) | 5g to 3,000g | 50g to 15,000g | Unlimited |
| Geometric Complexity | Extreme (3D undercuts, internal threads) | Moderate (2.5D axial pressing) | High (Thin walls, ribs, pockets) | High (Limited by tool reach) |
| Dimensional Tolerance | ±0.3% to ±0.5% (±0.05mm raw) | IT 8 - IT 11 (±0.02mm pressed) | ±0.1mm raw (±0.005mm CNC finished) | ±0.002mm to ±0.01mm |
| Material Density | 95% – 99% (Wrought equivalent) | 85% – 92% (Oil impregnable) | 100% Solid (Cast structure) | 100% Solid Wrought Stock |
| Surface Roughness (Ra) | 1.0 – 1.6 µm | 1.6 – 3.2 µm | 1.6 – 3.2 µm | 0.4 – 1.6 µm |
| Economic Production Run | > 2,000 pcs / year | > 5,000 pcs / year | > 2,000 pcs / year | 1 to 1,000 pcs |
3. Strategic Industry Solutions for Dutch High-Tech Ecosystems
JHMIM customizes its OEM supply capabilities to match the precise metallurgical and operational demands of key Dutch industrial corridors.
Brainport Eindhoven: Semiconductor & Precision Optics
The semiconductor supply network around Eindhoven demands sub-micron accuracy, ultra-clean materials, and extreme thermal stability. JHMIM provides specialized custom stainless steel (316L, 17-4PH) and titanium MIM brackets, kinematic mounts, and vacuum-compatible sensor housings. Parts undergo vacuum degreasing and ultrasonic cleaning to prevent outgassing in cleanroom environments.
Rotterdam Maritime & Offshore Wind Engineering
Offshore marine environments in the North Sea present intense saltwater corrosion challenges. We supply Dutch maritime clients with high-nickel alloy components, duplex stainless steel sintered filters, and heavy-duty anodized die-cast zinc/aluminum cable clamps and valve bodies designed to survive 1,000+ hours of ASTM B117 salt spray testing.
Wageningen & Westland: Agri-Robotics & Smart Greenhouses
Netherlands automated agriculture uses robotic pickers, sorting conveyors, and smart climate controls. JHMIM manufactures high-torque powder metallurgy planetary gears, timing pulleys, and copper-oil sintered sleeve bearings that operate maintenance-free in humid, high-dust greenhouse settings without requiring external grease replenishment.
Amsterdam & Utrecht: Urban E-Mobility & Smart Cargo Bikes
The Dutch light electric vehicle (LEV) and micro-mobility market demands ultra-compact drive-train parts. We mass-produce high-strength sintered internal gears, mid-drive motor brackets, and forged/cast aluminum brake levers, enabling lightweight design with long battery range and smooth mechanical operation.
4. Streamlined Procurement: Quality Assurance, Logistics & EU CBAM Alignment
Procuring custom parts across continents requires zero ambiguity regarding quality control, legal compliance, and freight predictability. JHMIM implements full-stack digital quality tracking and logistics integration tailored for Dutch importers.
IATF 16949 & ISO 9001 Certified QC
Every production batch undergoes First Article Inspection (FAI), in-process statistical process control (SPC), and 100% automated optical dimensional checking. Full measurement reports (CMM), material spectrometry certificates (ROHS/REACH chemical compliance), and heat treatment hardness curves are supplied with each consignment.
Direct Ningbo to Rotterdam Maritime Express
Located near Ningbo-Zhoushan Port (the world's largest cargo hub), JHMIM offers direct ocean freight shipping to the Port of Rotterdam (approx. 26 to 30 days transit). We support flexible IncoTerms including DDP (Delivered Duty Paid), DAP, and FOB, handling custom clearance, EU import tariffs, and inland transport directly to your warehouse in Brabant, Gelderland, or North Holland.
CBAM & ESG Carbon Traceability
To help Dutch clients comply with the European Union's Carbon Border Adjustment Mechanism (CBAM) regulations, JHMIM tracks embodied carbon intensity per kilogram of produced metal. Through energy-efficient vacuum sintering furnaces, closed-loop water recycling, and material scrap re-melting, we assist your ESG compliance reporting.
5. Design for Manufacturability (DFM) Guidelines for MIM & Sintering
Optimizing part geometry during early R&D phases prevents costly tooling revisions and reduces piece price by up to 40%. Our engineering team highlights core DFM rules for Dutch mechanical designers:
1. Uniform Wall Thickness & Coring Out
In MIM and Die Casting, abrupt changes in section thickness cause internal sink marks, voiding, and thermal distortion during sintering or cooling. Maintain uniform wall thickness between 1.0mm and 3.0mm. Core out thick sections using structural ribs, which preserve part strength while minimizing material weight and sintering cycle time.
2. Radii, Fillets & Internal Corner Chamfers
Sharp internal corners act as stress concentrators and can induce micro-cracking during thermal debinding and sintering. Incorporate generous fillets with a minimum radius of R = 0.5mm (R = 1.0mm preferred). Fillets improve powder feedstock flow during injection and extend mold die lifecycle significantly.
3. Draft Angles & Ejection Considerations
While MIM requires minimal draft angles compared to sand or investment casting, providing a 0.5° to 1.0° draft along draw directions facilitates smooth part ejection without pin marks or cosmetic distortion. For powder metallurgy (PM), axial surfaces should avoid undercuts perpendicular to the press direction.
4. Gate Placement & Sintering Support Surfaces
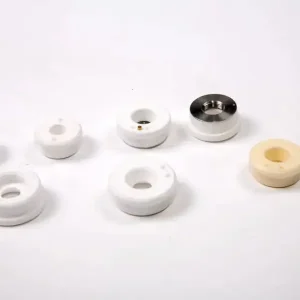
MIM parts shrink by approximately 15% to 20% during sintering in high-temperature hydrogen/argon atmospheres. Designs must feature a continuous flat surface or require custom ceramic setter plates for uniform support during thermal densification, maintaining tight flatness control (< 0.1mm).
Precision Sintered, MIM & Cast Components Series
Explore our proven manufacturing portfolio engineered for global OEM supply chain integration.




6. Frequently Asked Questions by Dutch Technical Buyers
Detailed answers addressing engineering validation, IP protection, delivery timelines, and regulatory compliance for European OEMs.
Partner with China's Premier OEM Engineering Specialist
Upload your 2D/3D component drawings today. Receive an engineer-reviewed Design for Manufacturability (DFM) assessment and an itemized cost estimate within 48 hours.