
Featured OEM Precision Components for London Buyers
Engineered to exact British Standards (BS/EN) with comprehensive DFM support, certified quality traceability, and rapid European delivery frameworks.




Greater London’s Industrial Landscape & OEM Supply Chain Realities
A Strategic White-Paper on Sourcing Precision Engineered Components for the UK's Premier Tech & Manufacturing Hubs.
London’s Advanced Manufacturing Renaissance
While London is globally renowned as a financial epicenter, Greater London and the surrounding Home Counties represent one of Europe's most dynamic advanced engineering corridors. Key industrial clusters—including the Thames Estuary Production Corridor, Park Royal industrial zone, and the "Golden Triangle" spanning London, Cambridge, and Oxford—are driving unprecedented demand for miniaturized, high-strength metal components.
From next-generation medical surgical robotics developed near King’s Cross Tech City to electric powertrain architectures engineered in South East England, original equipment manufacturers (OEMs) require component suppliers that can bridge extreme geometric complexity with rigid cost control.
Navigating Post-Brexit Supply Chain Friction
Procurement directors in the UK face multifaceted challenges following supply chain realignments. Compliance with UKCA (UK Conformity Assessed) markings, adherence to UK REACH chemical registration standards, and the mitigation of transatlantic tariff volatility mean that UK OEMs can no longer rely on fragile, multi-tiered supplier chains.
Ningbo Jiehuang Chiyang Electronic Tech Co., Ltd. (JHMIM) serves the London market by acting as a direct-to-factory partner. By unifying tool design, powder metallurgy, MIM, and high-pressure die casting under IATF 16949 oversight, we eliminate tier-2 markups and ensure total compliance with UK import metrics.
Manufacturing Process Matrix for UK Engineering Teams
Selecting the optimal route—MIM, Powder Metallurgy, Die Casting, or CNC Finishing—based on annual production volume, wall thickness, and alloy strength.
| Process Route | Ideal Annual Volume | Geometric Complexity | Typical Dimensional Accuracy | Surface Finish (Ra) | Key Material Options |
|---|---|---|---|---|---|
| Metal Injection Molding (MIM) | 2,000 – 1,000,000+ units | Extreme (Undercuts, internal threads, 3D curves) | ±0.3% to ±0.5% (Down to ±0.02mm) | 0.8 – 1.6 µm | 17-4PH, 316L, Ti-6Al-4V, Fe-Ni Alloys |
| Powder Metallurgy (PM) | 5,000 – 500,000+ units | Moderate (2.5D stepped profiles, structural gears) | IT 8 to IT 11 (High repeatability) | 1.6 – 3.2 µm | Sintered Steels, Copper-Steels, MPIF 35 Materials |
| High Pressure Die Casting (HPDC) | 2,000 – 200,000+ units | High (Thin-wall housings, cooling fins) | ±0.05mm – ±0.1mm | 0.8 – 3.2 µm | ADC12, A380, Zamak 3, Zamak 5 |
| 5-Axis CNC Machining | 1 – 2,000 units (Prototyping) | Limited by cutter tool accessibility | ±0.005mm – ±0.01mm | 0.4 – 1.6 µm | Wrought Aluminum, Stainless Steel, Brass |
17-4PH & 316L Stainless Alloys
Crucial for London’s medical device manufacturers and marine-grade outdoor fixtures along the Thames Corridor. Delivers wrought-like tensile strength exceeding 1,150 MPa after H900 heat treatment, combined with exceptional pitting corrosion resistance.
Titanium MIM (TiMIM) Breakthroughs
Targeted specifically at London's biotechnology research firms and aerospace actuators. Ti-6Al-4V components produced via Titanium MIM reduce weight by 45% compared to steel while maintaining bio-compatibility and extreme strength-to-weight ratios.
Die Cast Lightweighting (ADC12/Zamak)
For UK smart city infrastructure, EV charging hubs, and architectural lighting networks. High-pressure aluminum casting enables ultra-thin heat sink fins (down to 1.2mm) with superior thermal conductivity up to 96 W/m·K.
20+ Years of Metallurgical Mastery: Certified for European OEMs
How JHMIM enforces rigorous Quality Control (QC) and Design for Manufacturability (DFM) standards trusted across North America, Japan, and the United Kingdom.
Dual Quality Systems: ISO 9001 & IATF 16949
Quality isn't inspected at the end of our line; it is engineered into every stage of production. JHMIM operates an audited quality management structure holding both ISO 9001:2015 and automotive-grade IATF 16949:2016 certifications.
Our quality control lab is equipped with Japanese-imported coordinate measuring machines (CMM), optical profile projectors, x-ray porosity detectors, thermal conductivity analyzers, and salt-spray corrosion chambers. Every shipment bound for London includes a complete First Article Inspection (FAI) report and raw material heat certificates.
Patented R&D & Collaborative Innovation
Supported by 8 material invention patents and strategic research alliances with CAS Ningbo and Tianjin University, our senior engineering team brings unmatched technical depth to your project. Over 85% of our process development engineers possess more than 6 years of hands-on MIM powder binder development and mold design expertise.
When London design houses share 3D CAD models (STEP/IGES), our engineers perform a complimentary 48-hour DFM Review, flagging potential sink marks, parting line shifts, or draft angle deficits before mold steel is cut.
Future-Proofing OEM Component Supply for the UK Market
How JHMIM is deploying AI-assisted mold cavity flow simulation, green sintering technologies, and rapid prototyping integration to transform European procurement.
01. AI Flow Simulation
By simulating powder binder separation and thermal shrinkage vectors using neural network flow models, we reduce mold trial iterations from 4 down to 1, cutting sample lead times for London clients by over 35%.
02. Hydrogen Sintering
Aligned with the UK's stringent Net-Zero 2050 targets, our upgraded continuous mesh belt furnaces utilize low-carbon hydrogen atmosphere sintering to lower embodied carbon in finished MIM and PM parts.
03. Direct Metal 3D Printing
Bridging sample prototyping and high-volume injection tooling. We offer direct metal laser sintering (DMLS) prototypes in 3–5 days, allowing London design engineers to conduct physical testing before tooling commitment.
Frequently Asked Questions by UK Procurement Managers
Clear, direct answers regarding non-disclosure agreements, lead times, logistics to London ports, and tooling ownership.
Can JHMIM execute a mutual Non-Disclosure Agreement (NDA) before reviewing IP drawings?
Yes, absolutely. We regularly sign NDAs with UK design studios, university spinoffs, and tier-1 industrial firms prior to receiving 2D PDF or 3D STEP drawings. All project data is stored on air-gapped secure servers accessible only by dedicated project engineers.
What are the standard shipping timelines and logistics options to Greater London?
We offer flexible Incoterms including DDP (Delivered Duty Paid), DAP, and FOB. Air freight via London Heathrow (LHR) takes 5–7 business days for urgent pilot production, while sea freight through Port of Tilbury or London Gateway typically spans 28–35 days for high-volume shipments.
Who retains ownership of the custom injection molds or die casting dies?
The client retains 100% legal ownership of all custom tooling paid for by the customer. Molds are maintained at our certified facility under strict temperature-controlled storage and guaranteed for up to 500,000 shots at zero additional maintenance cost to the client.
What are your Minimum Order Quantities (MOQ) across different process lines?
Our standard production MOQs are tailored to industrial manufacturing economics: 2,000 pieces for Metal Injection Molding (MIM) parts, 2,000 pieces for CNC finishes and aluminum die castings, and 5,000 pieces for sintered powder metallurgy components. Initial prototype and pilot runs are supported via Metal 3D Printing.
How does MIM achieve 30%–50% cost savings compared to traditional 5-axis CNC machining?
CNC machining creates complex shapes by subtractive cutting, generating significant material waste (often up to 70% scrap) and lengthy machine tool runtimes. MIM is an additive near-net-shape process that injects feedstock into multi-cavity molds with minimal waste, making it dramatically cheaper for volumes above 2,000 units.
Expanded OEM Precision Product Line for UK & European Industry
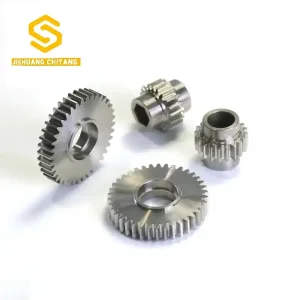
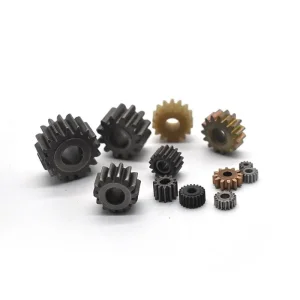
Explore our complete range of sintered gears, micro-components, stainless steel porous filters, laser ceramics, and precision MIM assemblies.





Accelerate Your Engineering Project in London
Send us your STEP CAD drawings or 2D technical specifications. Receive an itemized factory-direct quotation and a comprehensive engineering DFM evaluation within 48 hours.
Send Inquiry Now