
Berlin Industry OEM Precision Sintered Parts
Direct manufacturer supply of ISO/IATF 16949 certified powder metal components customized for the Berlin-Brandenburg industrial region.

Precision Sintered Steel Structural Components for Berlin Industrial Automation
High-density sintered iron-copper-carbon alloy parts designed for heavy-duty drive mechanisms and robotics in Berlin-Brandenburg manufacturing facilities.
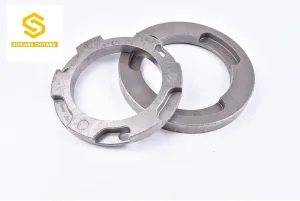
High-Torque PM Powertrain Sintered Components for E-Mobility & Automotive
Engineered for dynamic stress resistance, wear longevity, and acoustic dampening across Berlin urban mobility vehicles and motorcycle assemblies.

Custom DIN Class 7-9 Precision Metal Powder Metallurgy Gears
High-volume spur, helical, and planetary gear sets engineered with micro-alloyed nickel steels for electric actuators and power tools.

Custom Alloy Steel Machinery Sintered OEM Automotive Components
Precision-sintered valve train components, sensor housings, and transmission linkages delivering 35% material cost savings vs. CNC machining.
The Powder Metallurgy Landscape in the Berlin-Brandenburg Region
Decoding supply chain demands, green technology shifts, and advanced metal forming adoption across Germany’s capital industrial hub.
Berlin’s Industrial Metamorphosis & Near-Net-Shape Demand
The Berlin-Brandenburg industrial corridor has experienced a massive technology-driven renaissance. Known historically for electrical engineering and heavy machinery (anchored by industrial estates like Siemensstadt Square and Adlershof Science Park), the region has transformed into Europe’s premier electro-mobility and high-tech manufacturing axis. The rapid growth of gigafactories, clean-tech startups, and medical technology enterprises in Berlin has shifted procurement priorities toward zero-waste, energy-efficient manufacturing processes.
Conventional subtractive manufacturing (CNC milling and turning) poses severe challenges for Berlin tier-1 suppliers due to high electricity costs, raw material scrap rates exceeding 40%, and extended lead times. Powder Metallurgy (PM) and Metal Injection Molding (MIM) provide an essential solution: net-shape or near-net-shape processing that achieves up to 95% material utilization while drastically scaling throughput for complex structural geometry.
Global OEM Procurement Intent & Sourcing Challenges
Procurement directors and chief metallurgists within Berlin’s automotive, aerospace, and MedTech sectors face strict performance metrics. Key sourcing requirements include:
- Strict Mechanical Properties: Minimum tensile strengths up to 850 MPa and density levels exceeding 7.2 g/cm³ for load-bearing gears.
- Dimensional Repeatability: CPK ≥ 1.33 across high-volume production batches (50,000 to 1,000,000+ units annually).
- Decarbonized Supply Chain: Alignment with EU Green Deal regulations, requiring low-carbon sintering atmospheres and certified recycled metal powders.
- Accelerated Prototyping: Rapid DFM (Design for Manufacturability) verification and metal 3D printing prototyping prior to final press & sinter tooling production.
Materials Science Matrix: Press & Sinter vs. MIM
Comparing physical properties, alloy formulations, and structural standards (DIN ISO 5755 vs. MPIF Standard 35) for procurement teams.
| Technology Route | Common Materials & Standards | Achievable Density | Tensile Strength (UTS) | Geometric Complexity | Optimal Order Volume |
|---|---|---|---|---|---|
| Conventional Press & Sinter (PM) | Fe-Cu-C, Fe-Ni-Mo (DIN Sint-D11 to E30, MPIF FC-0208, FN-0205) | 6.8 - 7.3 g/cm³ | 350 - 750 MPa | Moderate (2.5D pressing direction features, stepped shafts, external gears) | 5,000 – 1,000,000+ pcs |
| Metal Injection Molding (MIM) | 316L, 17-4PH, 4140, Titanium Grade 5 (Ti-6Al-4V), Fe-Ni alloys | 7.5 - 7.85 g/cm³ (96-99% theoretical) | 750 - 1,150 MPa | Extreme (3D complex shapes, internal threads, undercuts, micro-holes) | 2,000 – 500,000+ pcs |
| High-Density Warm Compaction | Pre-alloyed diffusion bonded steel powders (Sint-F20) | 7.3 - 7.5 g/cm³ | 650 - 950 MPa | High (Helical gear teeth, high-load hydraulic pump rotors) | 10,000+ pcs |
| Ceramic Injection Molding (CIM) | Zirconia (ZrO₂), Alumina (Al₂O₃) | 5.9 - 6.05 g/cm³ | 1,200+ MPa (Flexural) | High (Ultra-wear resistant nozzles, medical insulators, watch bezels) | 2,000+ pcs |
Atmosphere-Controlled Sintering
Continuous mesh-belt furnaces utilizing 90% N₂ / 10% H₂ reducing atmospheres with continuous dew-point monitoring (-50°C) eliminate intergranular oxidation, ensuring consistent hardenability across all batch runs.
Post-Sintering Enhancements
Full in-house secondary operations including resin vacuum impregnation, steam oxidation (blackening), CNC precision grinding, hard case carburizing, and PVD coating for extreme friction applications.
Metrology & Microstructure
Zeiss 3D Coordinate Measuring Machines (CMM), optical profilometers, metallographic pore analysis software, and automatic magnetic particle crack detection guaranteeing zero-defect delivery to German plants.
Macro Sector Powder Metallurgy Solutions for Berlin OEMs
Specialized sintered metal architectures customized for key industrial sectors in Berlin and broader European supply chains.
E-Mobility & Powertrain Systems
Supplying high-density sintered oil pump rotors, electronic park-lock gears, variable valve timing (VVT) rotors, and electric drive motor stator cores. Optimized for high rotational fatigue life and minimal acoustic gear hum.
Medical & Surgical Technology
Fabricating 316L and Titanium MIM micro-components for laparoscopic endoscopic articulation jaws, bone staplers, and surgical instrument handles. Offering full biocompatibility, passivation compliance, and pass-through autoclave endurance.
Industrial Automation & Power Tools
Heavy-duty planetary gearboxes, bevel gears, ratchets, and quick-change lock mechanism components for industrial power tools and automated conveyor drives deployed in modern Berlin warehouse facilities.
German Supply Chain Compliance & Risk Mitigation
Ensuring seamless integration into Berlin OEM vendor matrices with comprehensive international standards verification.
IATF 16949 & ISO 9001 Audited Operations
Full APQP documentation, PPAP Level 3 submissions, FMEA risk assessments, and VDA 6.3 process audit readiness standard for every order.
EU REACH, RoHS & CBAM Transparency
100% compliant raw material sourcing with complete SVHC disclosure and Carbon Border Adjustment Mechanism (CBAM) carbon accounting paperwork.
Localized Logistics & Buffer Stocking
Direct door-to-door DDP logistics via Berlin Brandenburg Airport (BER) air freight or Hamburg seaport rail routing, supported by safety stock agreements.
Total Cost of Ownership (TCO) Calculator
Why Berlin engineers transition from CNC machining to Powder Metallurgy:
Technology Roadmap: Next-Gen Powder Metallurgy
Pioneering innovations in powder metal forming driving Berlin’s industrial modernization through 2030.
Super-Alloy Sintering (>1280°C)
Transitioning from standard 1120°C furnaces to 1300°C ultra-high temperature sintering allows complete pore closure and spheroidization, elevating dynamic impact toughness to match wrought alloy levels.
PM + Metal 3D Printing Co-Production
Combining mass-produced powder sintered blanks with laser powder bed fusion (LPBF) micro-features for custom aerospace and prototype batches destined for Brandenburg flight test centers.
Hydrogen-Reduced Metal Powders
Utilizing 100% green-hydrogen reduced iron powders to provide Berlin customers with near-zero embodied carbon components that fulfill strict corporate Scope 3 emission mandates.
Frequently Asked Questions for Berlin Buyers
Detailed answers to technical, commercial, and logistics questions submitted by engineering and sourcing professionals.
How does Jiehuang handle non-disclosure agreements (NDAs) and IP protection for proprietary Berlin technology drawings?
We routinely execute legally binding NDAs under European jurisdiction prior to receiving CAD geometry or STEP files. All customer engineering data is isolated on secure, encrypted internal servers with strict role-based access control to guarantee total protection of your intellectual property.
What minimum order quantities (MOQ) apply for press & sinter versus MIM components delivered to Germany?
For conventional Powder Metallurgy press & sinter parts, standard batch MOQs start at 5,000 pieces due to press setup and compaction die calibration. For Metal Injection Molding (MIM), the MOQ is 2,000 pieces. Pilot quantities and prototype sample batches can be arranged for early-stage evaluation.
Can Jiehuang match German DIN standard materials like DIN ISO 5755 or Sint-F20?
Yes. Our metallurgical laboratory cross-references international powder standards seamlessly. We match DIN ISO 5755 (e.g., Sint-D11, Sint-C10, Sint-E30), MPIF Standard 35, and JIS Z 2550 specifications. Chemical spectrum certificates and mechanical test data accompany every shipment.
What lead time can Berlin customers expect for production tooling and initial samples?
Standard tooling fabrication (compacting dies or MIM injection molds) and first article inspection (FAI) sample delivery require approximately 25 to 30 business days. Accelerated rapid-tooling and 3D printed metal prototype options are available within 7 to 10 days for design validation.
How does Jiehuang ensure dimensional consistency and prevent cracking in high-stress gears?
We employ closed-loop multi-stage CNC compaction presses with real-time pressure feedback to guarantee uniform core density. Post-sintering, parts undergo 100% automated optical sensor sorting, magnetic particle flaw detection, and ultrasonic density testing to eliminate micro-cracks before dispatch.
Full OEM Powder Metallurgy & MIM Product Portfolio
Explore our expanded range of precision metal solutions designed for Berlin industrial applications.

High-Precision Micro MIM Gear Structural Components
Complex metal injection molded structural gears engineered for fine-pitch actuator gearboxes in medical devices and robotics.

Custom Sintered Titanium (TiMIM) High-Strength Components
Ultra-lightweight, corrosion-resistant titanium injection molded parts tailored for aerospace and specialized automotive systems.

High-Precision Mechanical Sintered Cams & Levers
Custom engineered 3D profile powder metal cams designed for high-cycle industrial automation and assembly line machinery.
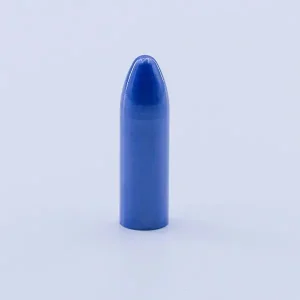
Sintered Technical Ceramics (CIM) Structural Components
Extreme wear resistance and dielectric isolation parts fabricated from high-purity zirconia and alumina for harsh environments.
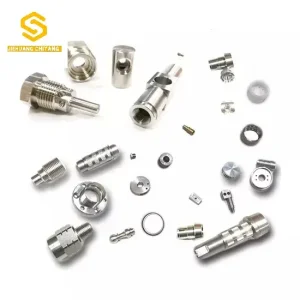
Industrial Grade MIM Stainless Steel Mechanical Parts
Near-net-shape 316L and 17-4PH stainless steel hardware providing exceptional tensile strength and fluid resistance.
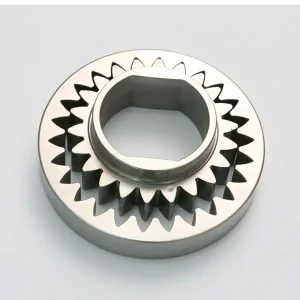
Automotive Powertrain Sintered Oil Pump Gears
High-density fluid displacement sintered gears featuring optimized tooth geometries for low noise and hydraulic efficiency.

Precision Gerotor & Sintered Oil Pump Rotors
Matched inner/outer rotor sets with micron-level clearance control for engine lubrication and transmission oil delivery.
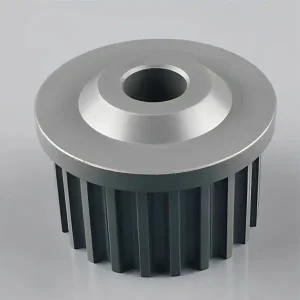
Powder Metallurgy Engine Water Pump Pulleys
Balanced, lightweight sintered belt drive pulleys built to resist thermal cyclic fatigue across commercial vehicles.
Accelerate Your Berlin Sintered Metal Project Today
Send your CAD drawings (STEP/IGES/PDF) to our chief engineering team. Receive an engineer-reviewed DFM report and a transparent quotation within 48 hours.